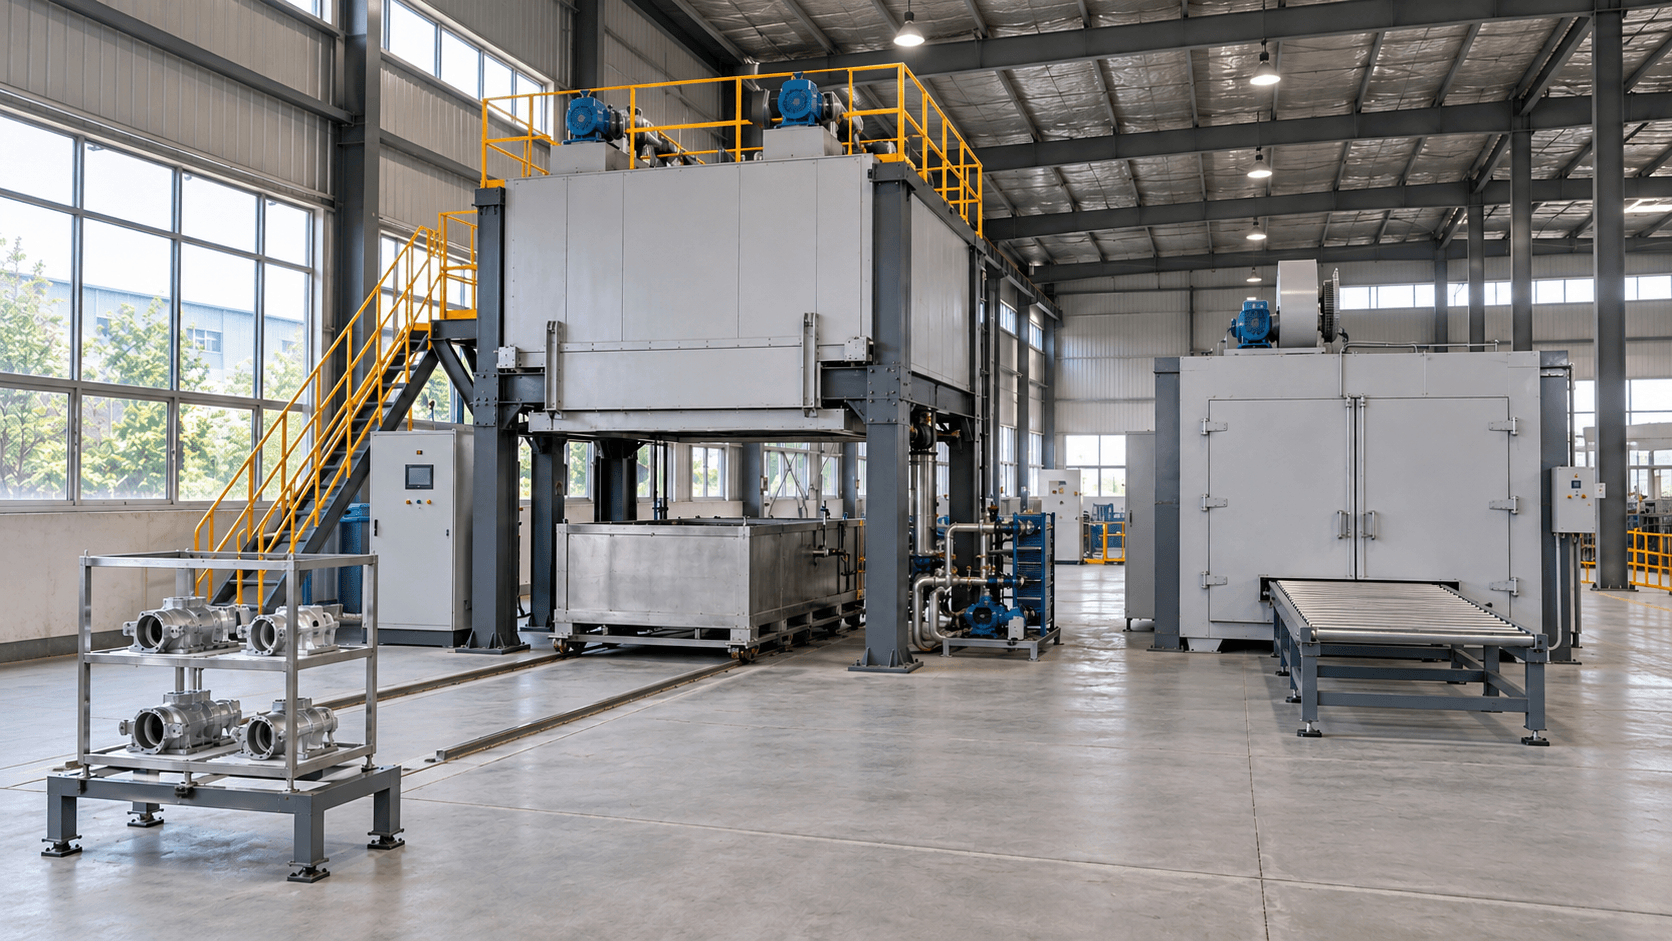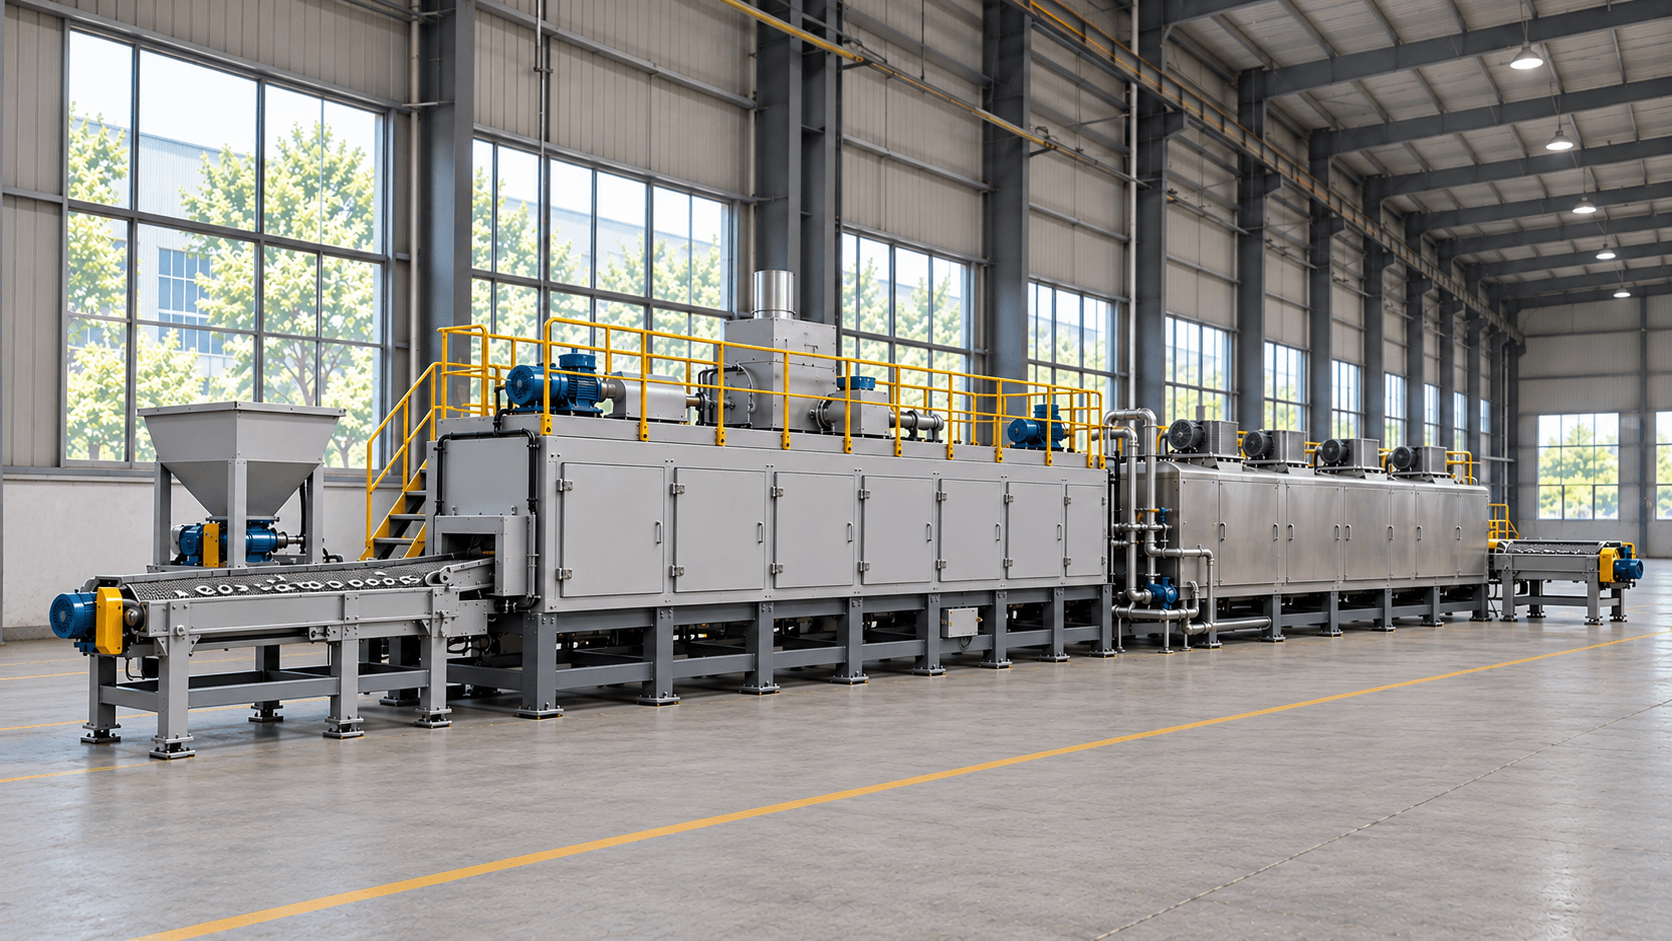
Continuous Mesh Belt Annealing & Tempering Line
For: Small and medium steel parts suitable for stable belt loading
Continuous annealing or tempering of quenched parts

Loading page…
Loading is taking longer than usual. Please wait or try again.
Retry loading
Select a heat-treatment line or individual furnace by workpiece, handling method and production cycle.
Find the line for your workpiece and process requirements
For: Small and medium steel parts suitable for stable belt loading
Continuous annealing or tempering of quenched parts
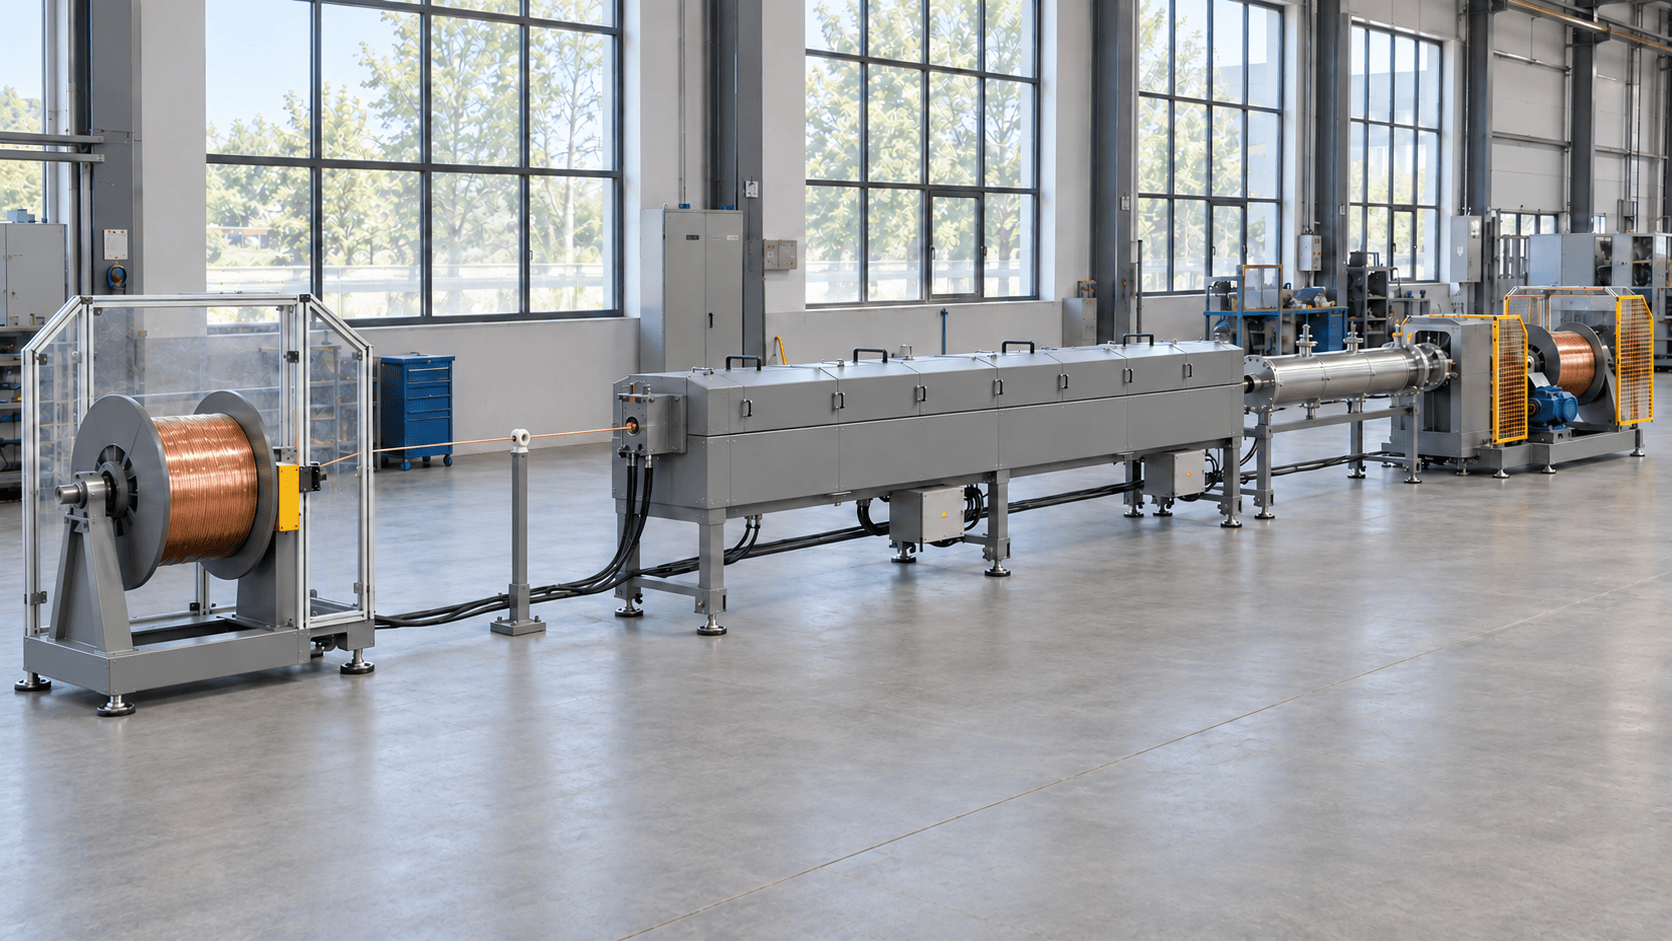
For: Copper and suitable copper-alloy wire
Continuous annealing · Protected cooling
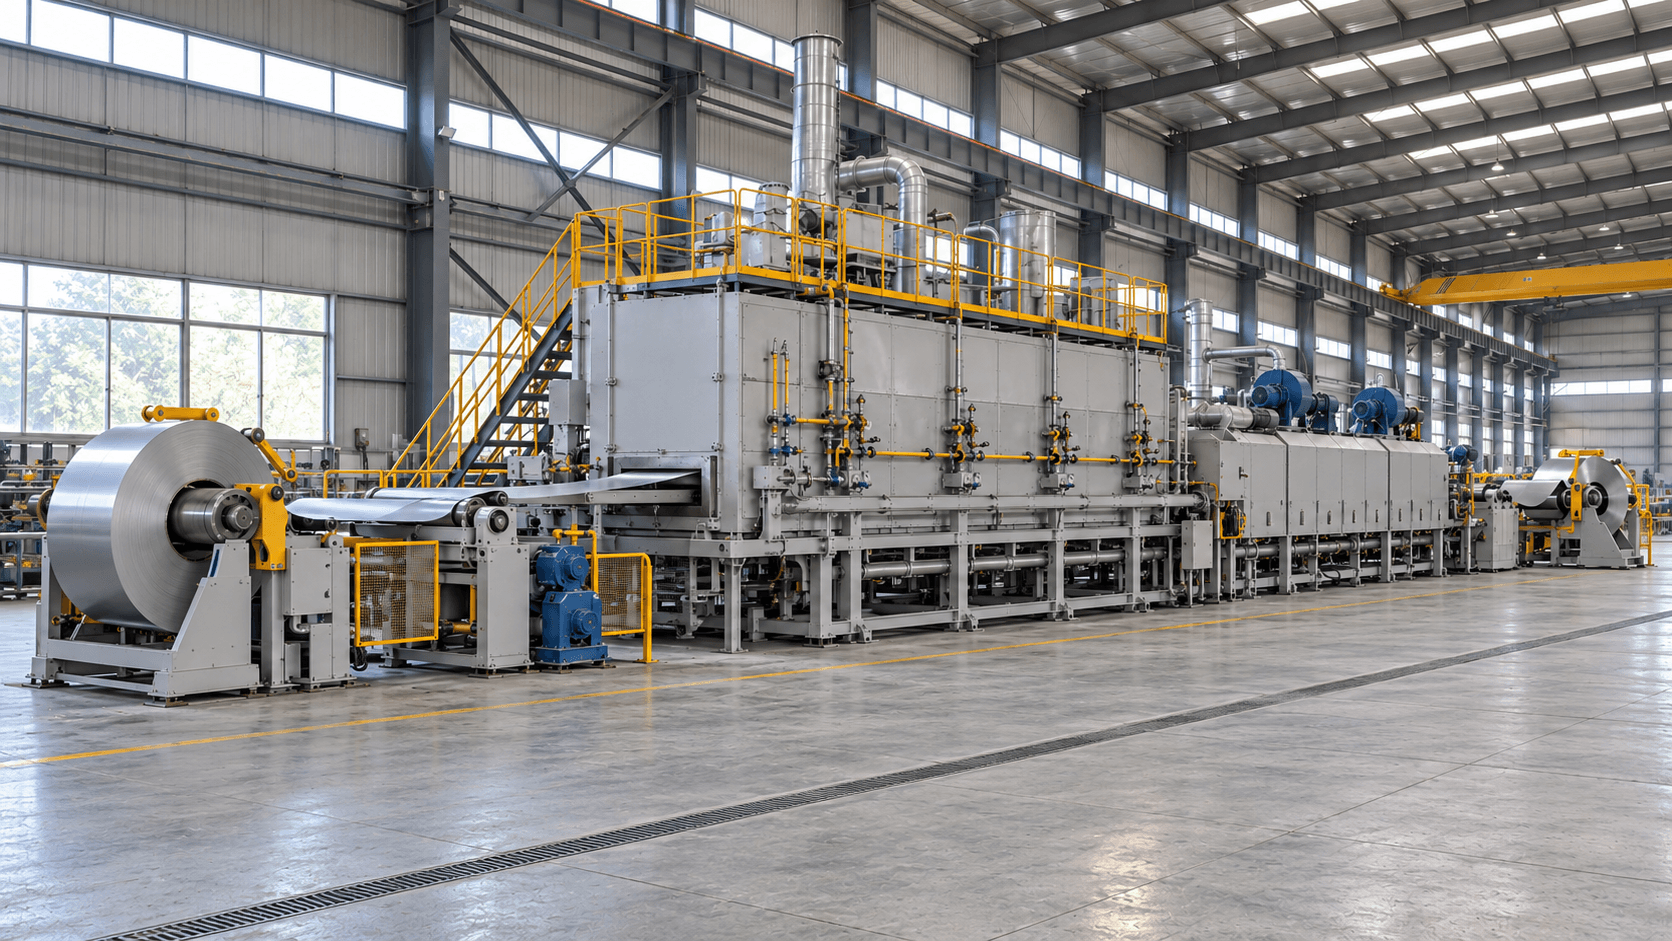
For: Stainless steel and suitable alloy strip
Annealing or solution treatment · Controlled cooling
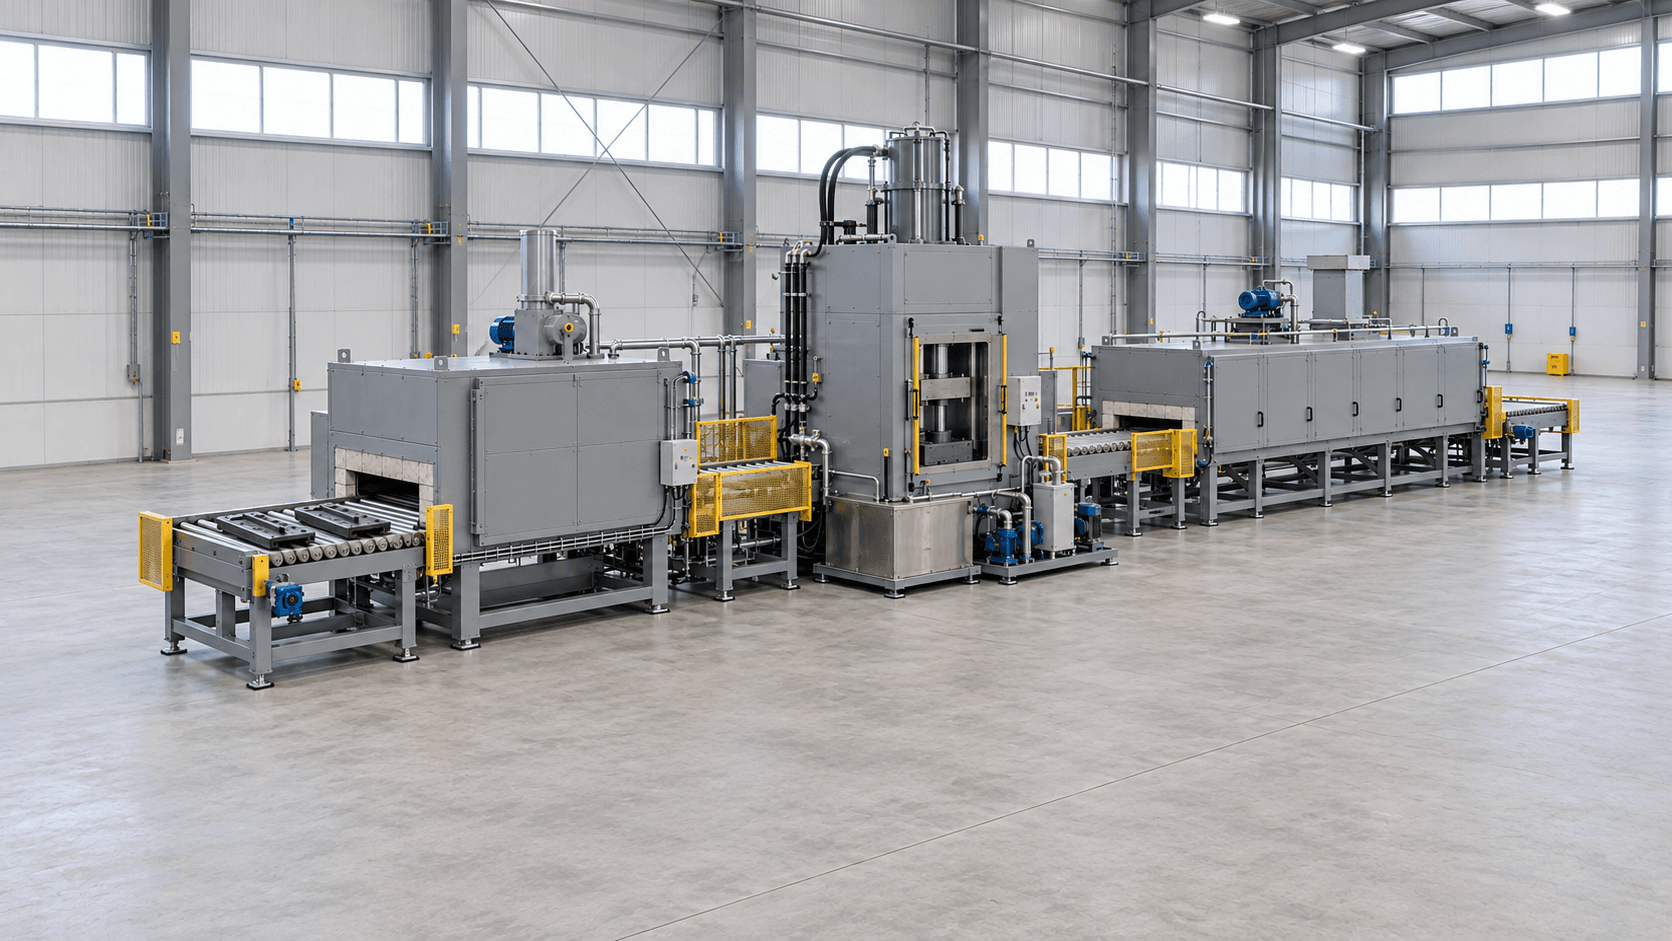
For: Track shoes with repeatable geometry and defined distortion limits
Heating · Press quenching · Tempering
For: Steel forgings validated for residual-heat quenching
Residual-heat quenching · Tempering
For: Steel fasteners requiring quenching and tempering
Quenching · Tempering
For: Small steel parts with defined case-depth requirements
Carburizing · Quenching · Tempering
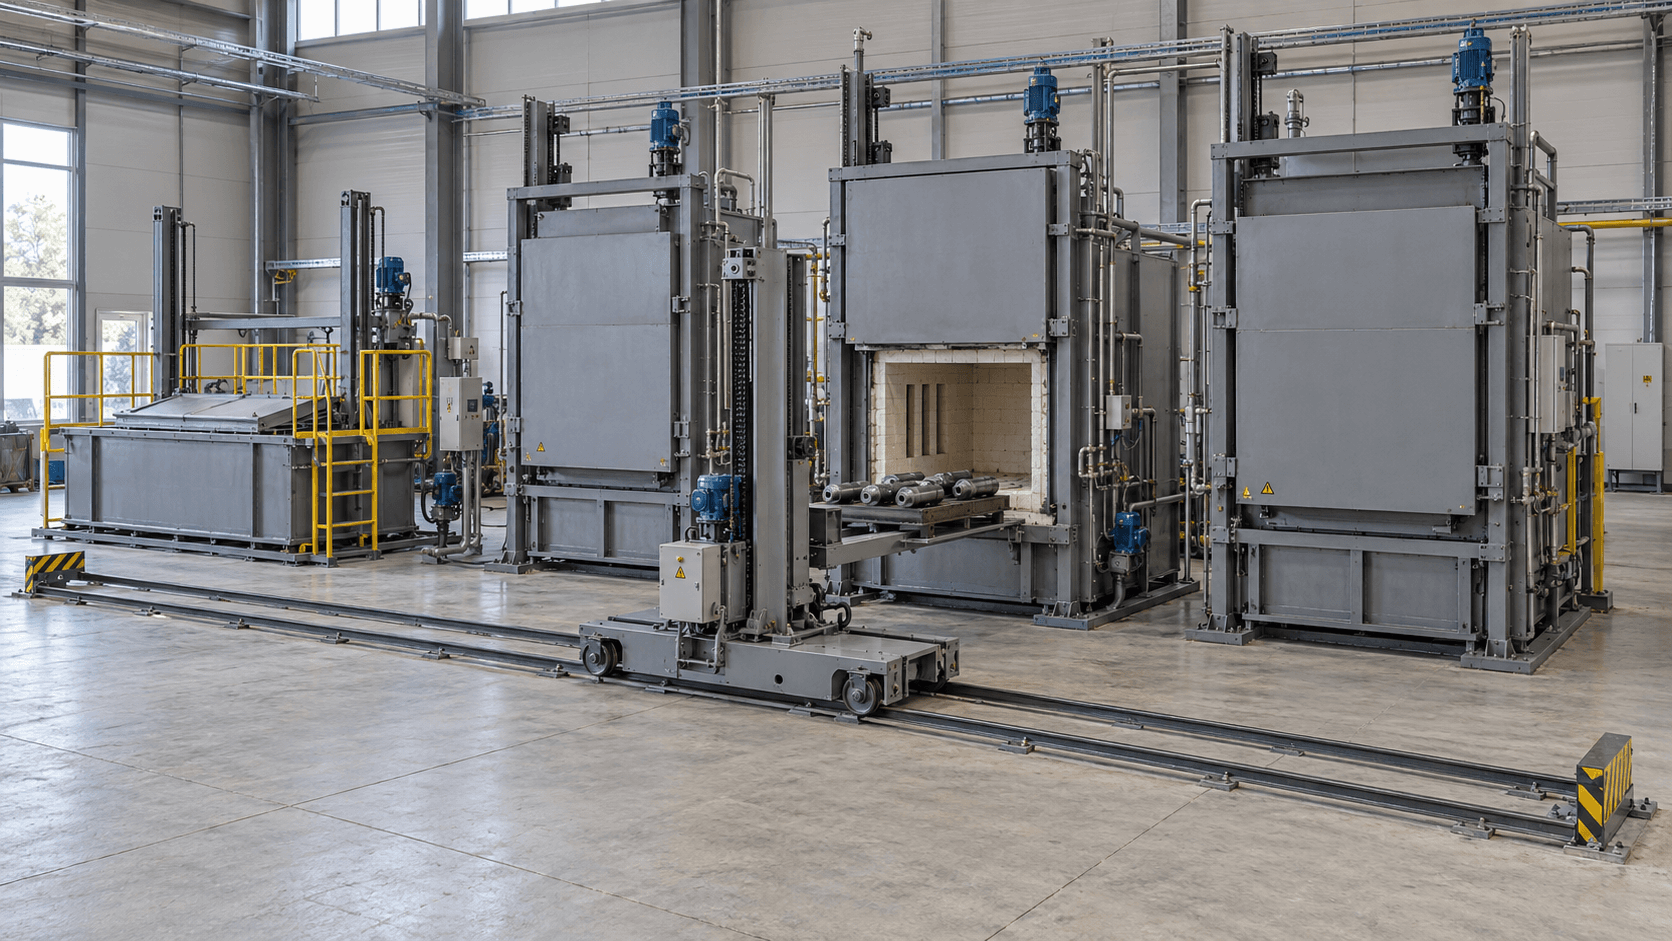
For: Workpieces from multiple furnaces with coordinated discharge windows
Separate furnace heating · Transfer & quench
For: Aluminum alloy parts suitable for solution treatment and aging
Solution treatment · Quenching · Artificial aging
For: Billets with a defined alloy grade and forging temperature window
Zoned heating · Equalizing · Exit temperature checks
For: Composite cylinders with defined resin systems and curing profiles
Heating · Curing soak · Cooling
Charge and discharge by batch
General heat treatment for small and medium workpieces and short production runs.
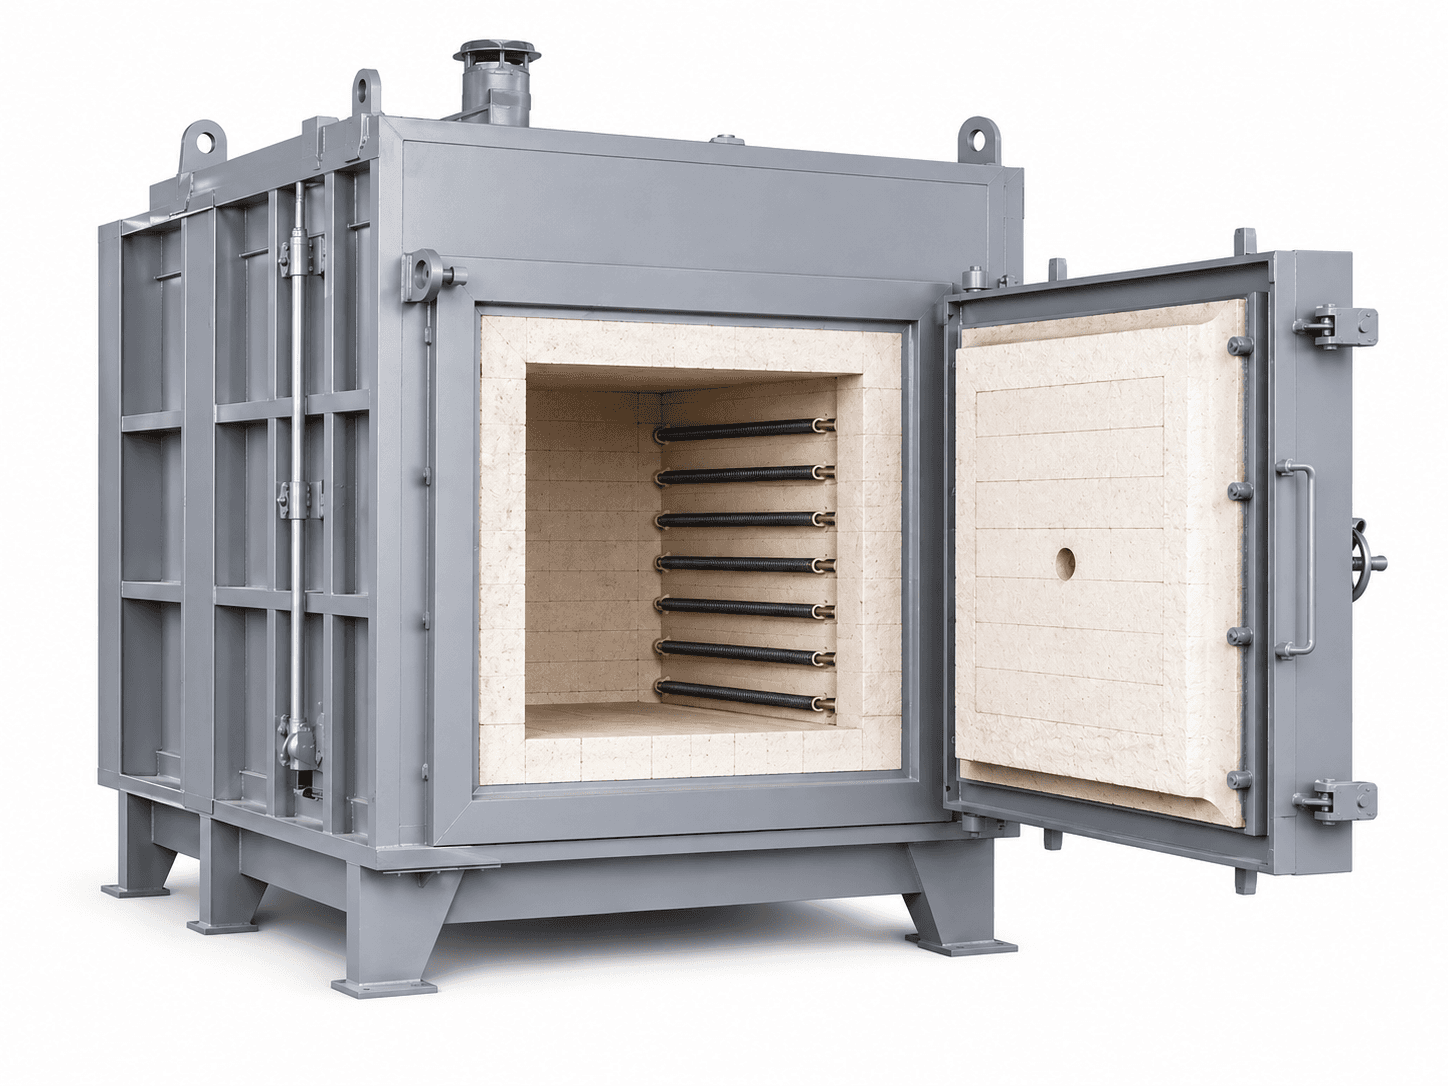
Batch heat treatment for large and heavy workpieces with trolley loading.
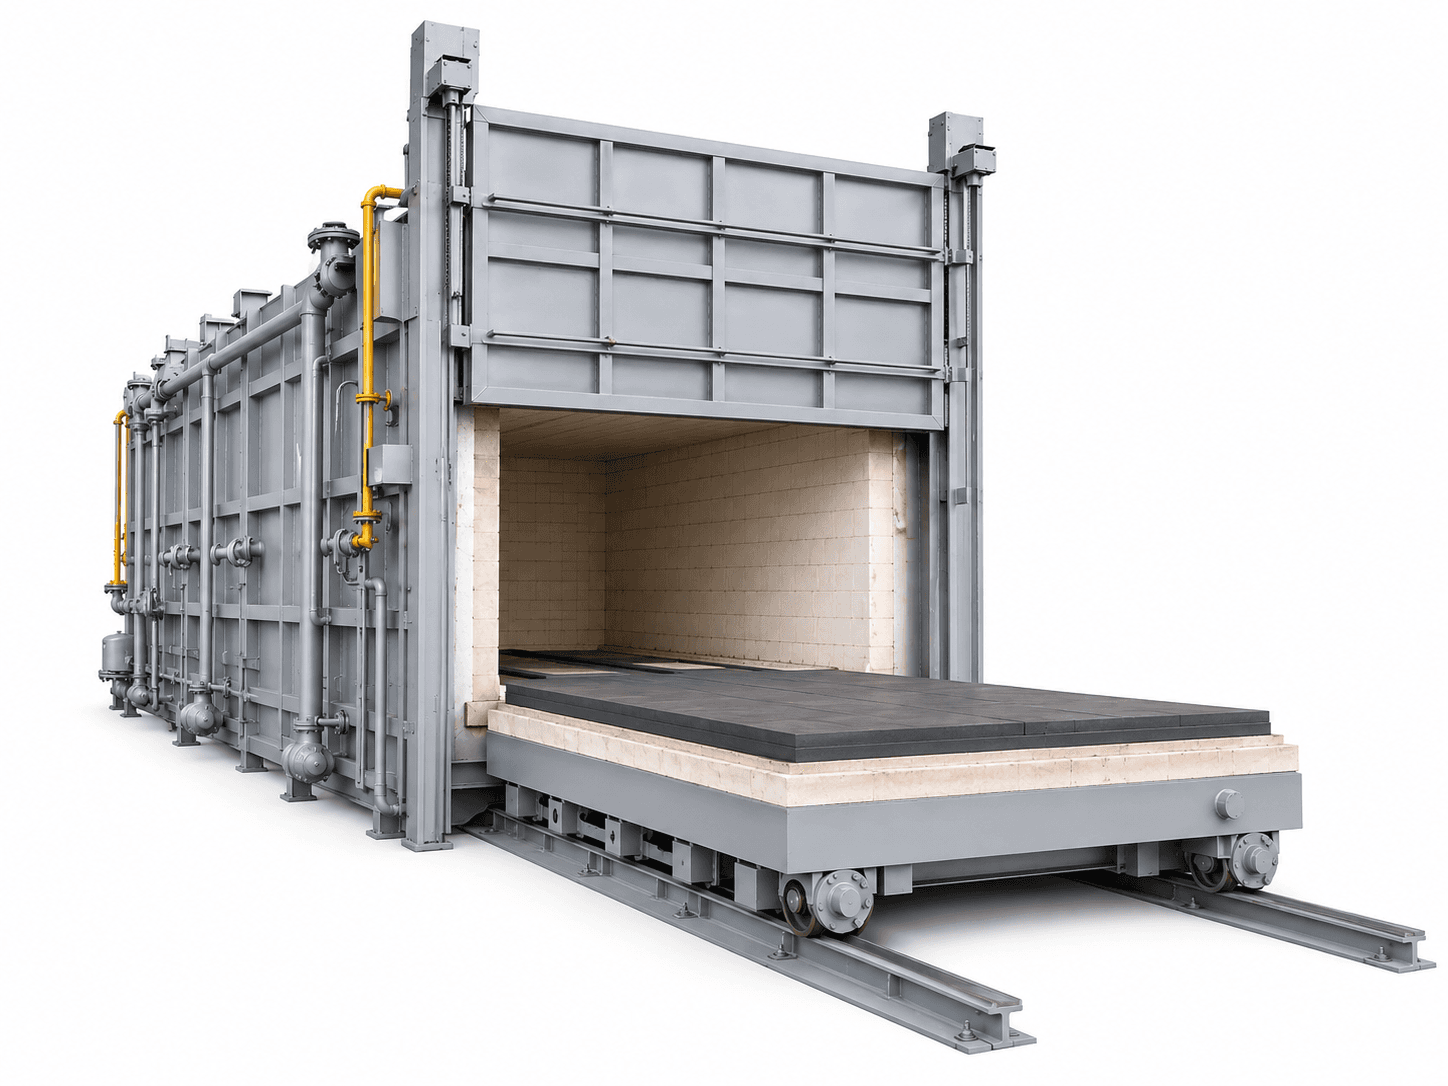
Vertical heat treatment for shafts, rods and other long workpieces.
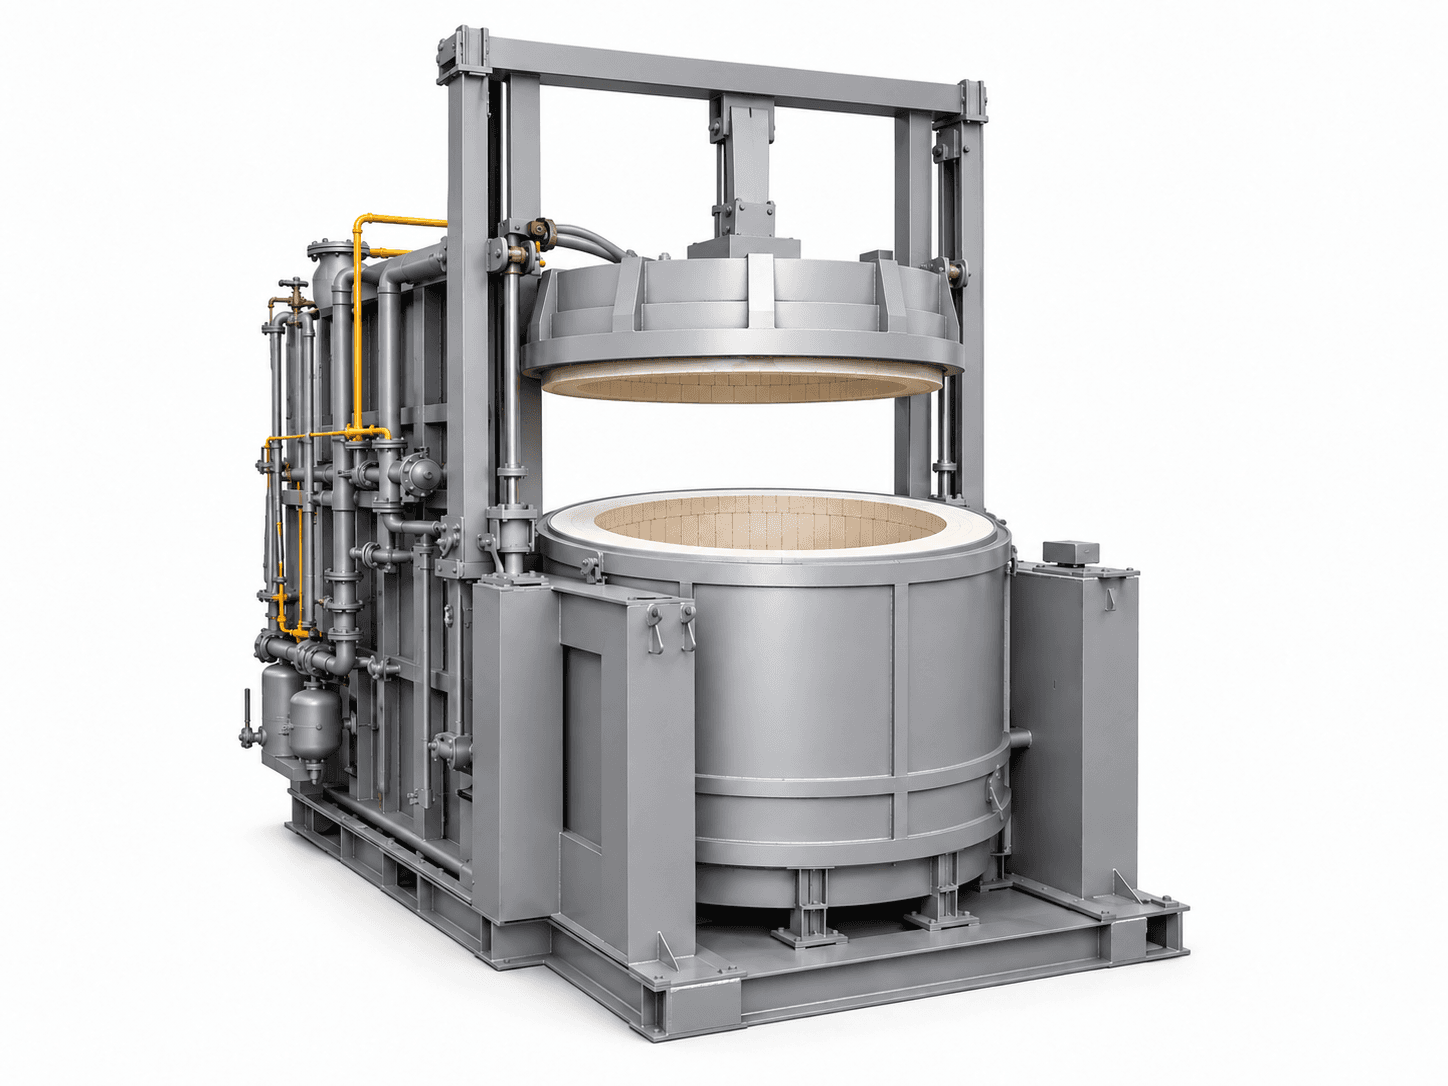
Batch and protective-atmosphere heat treatment for coils, wire and stacked loads.
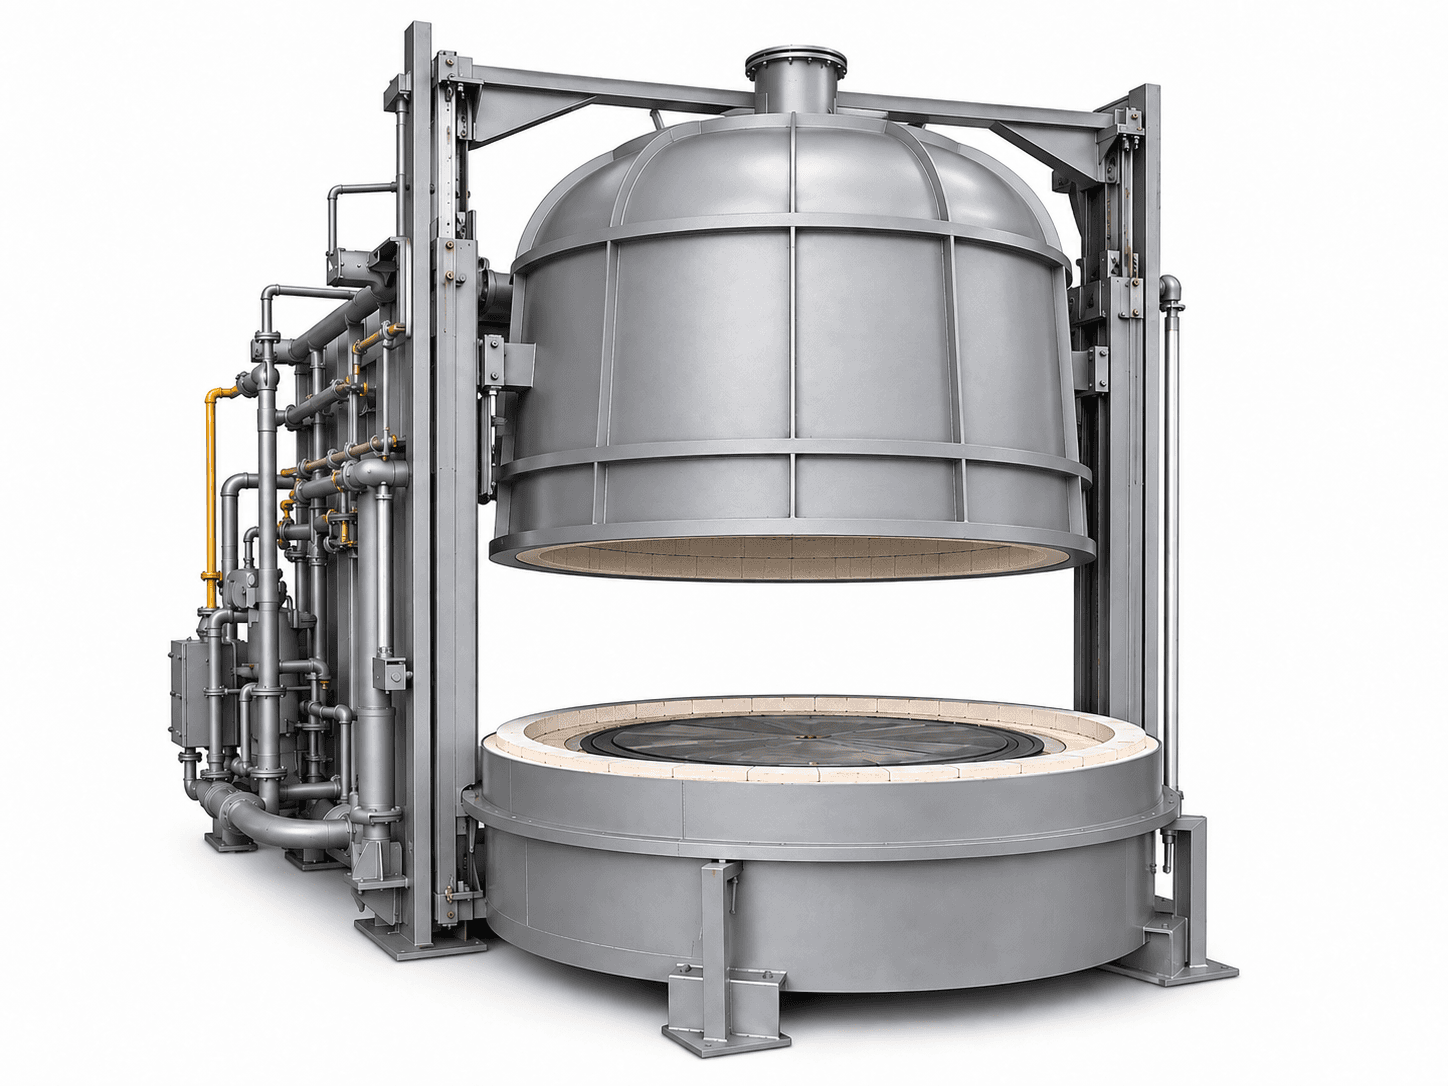
Batch heating with fork handling and coordinated transfer.
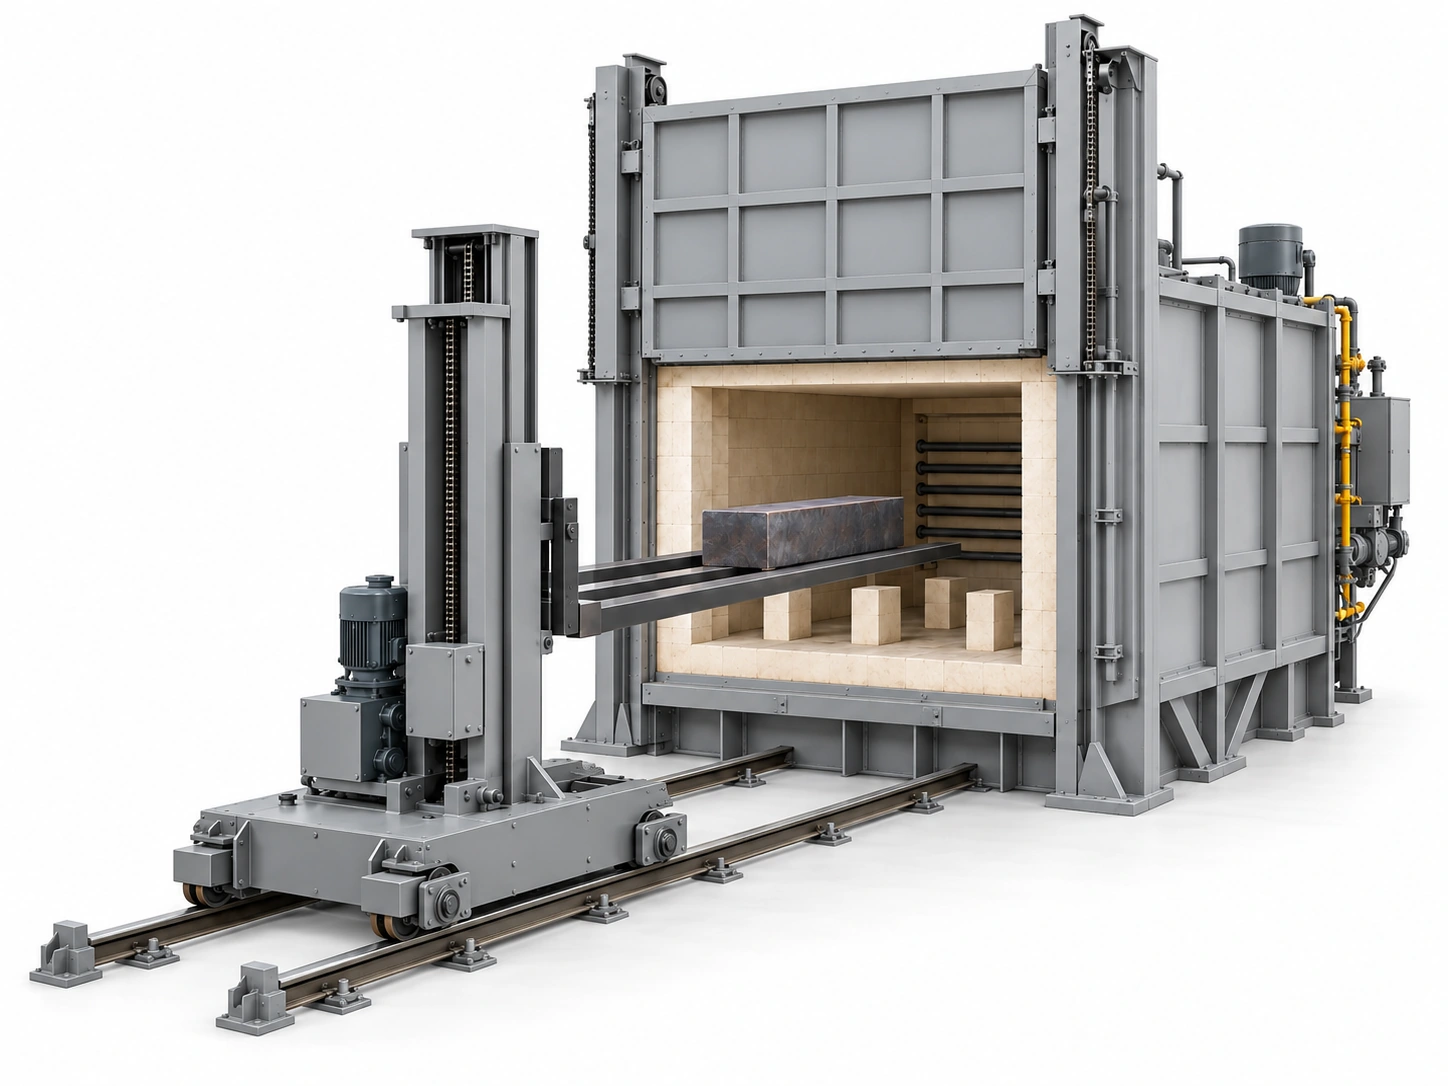
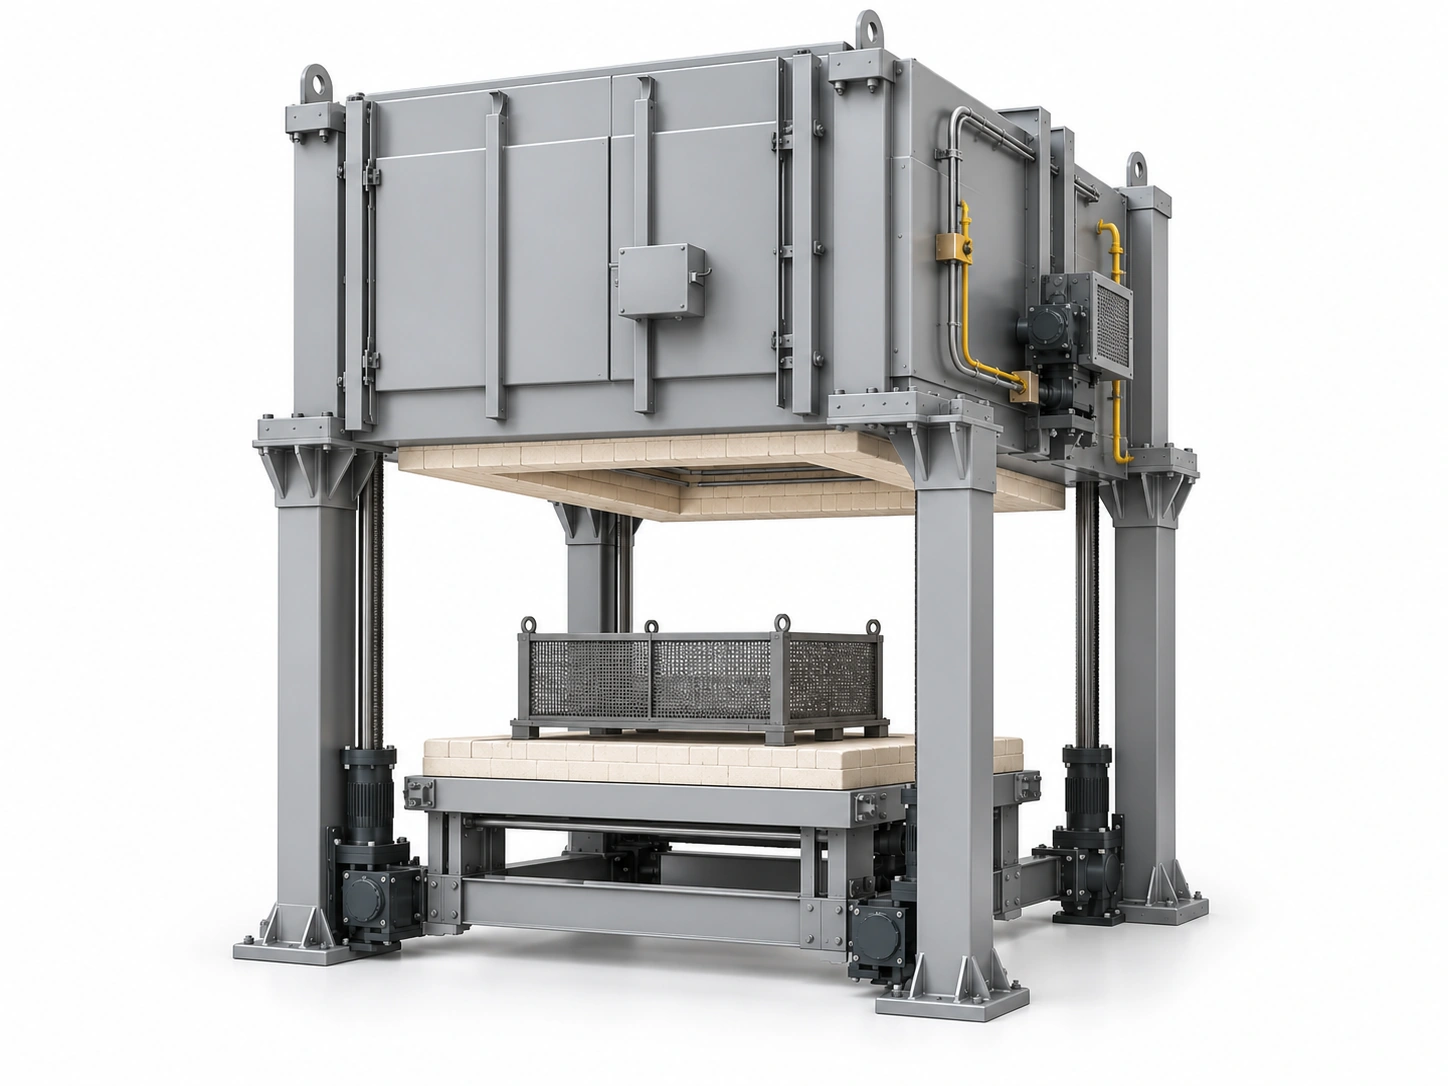
Batch heat treatment with an elevating loading hearth.
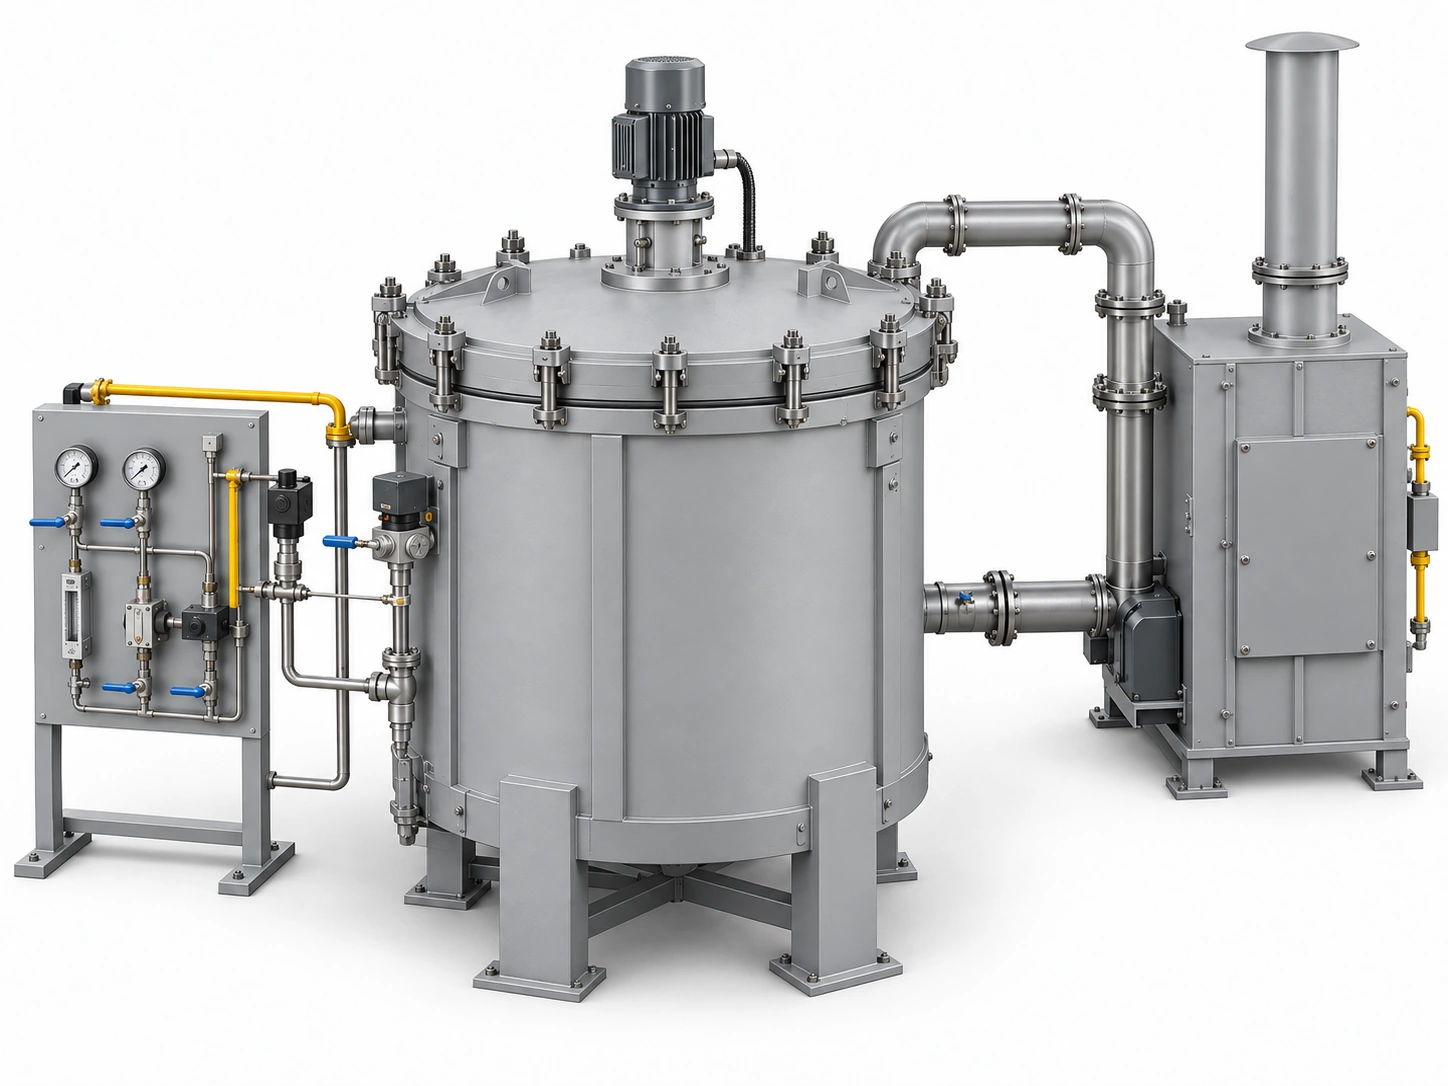
Batch gas nitriding for suitable steel components.
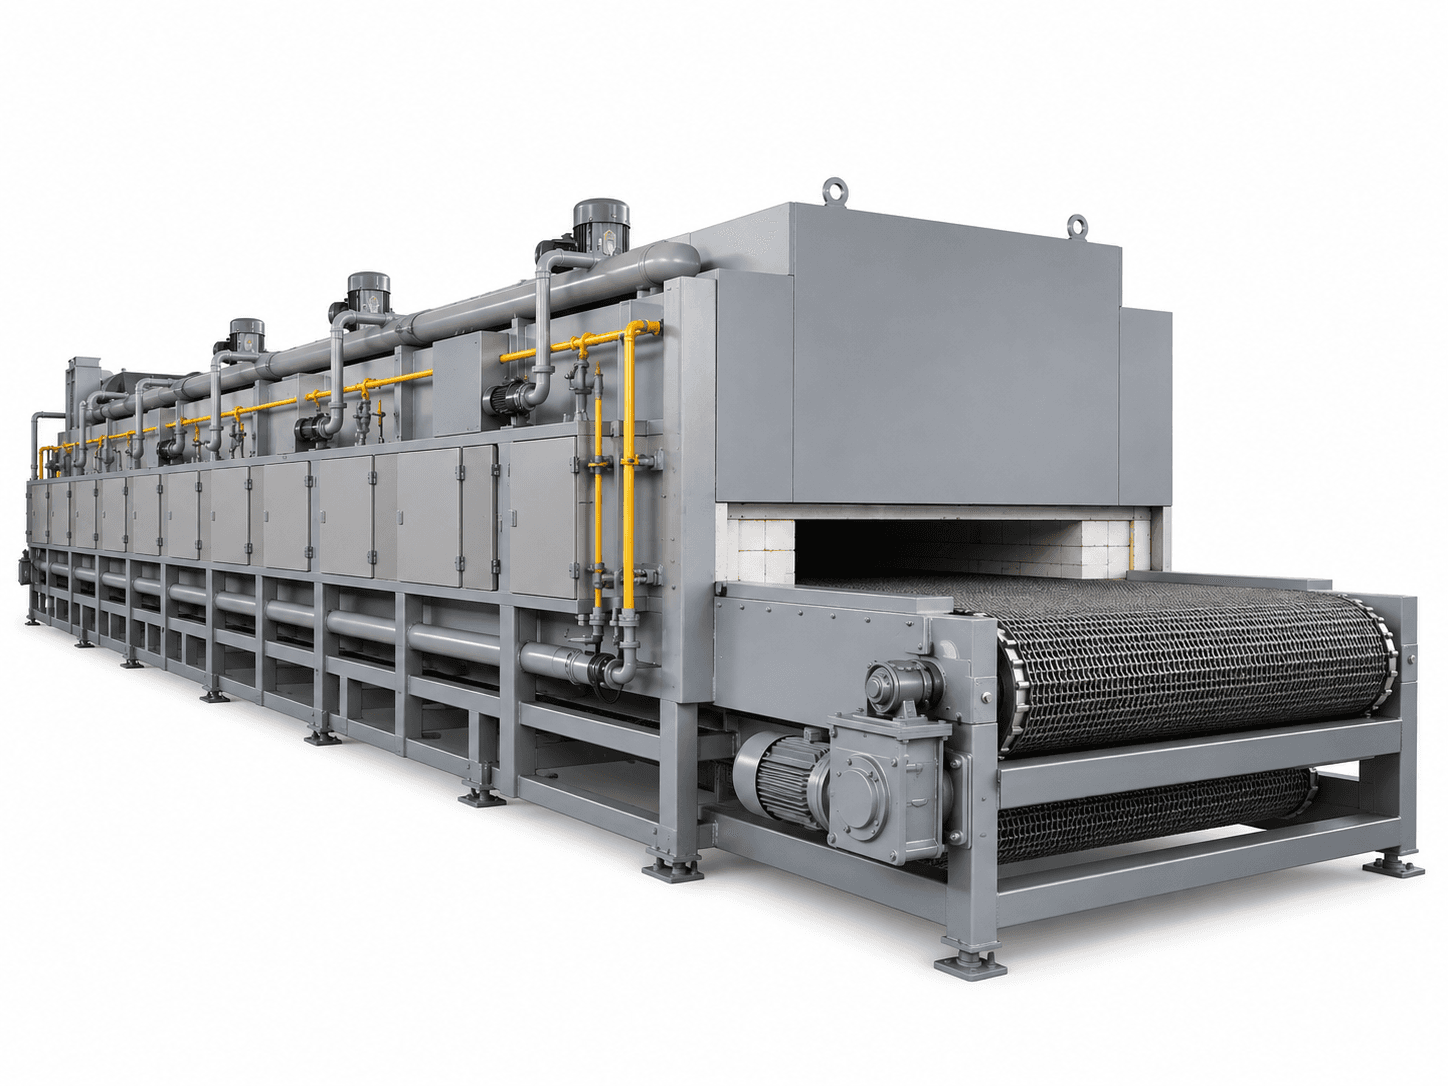
Workpieces pass through the furnace at a controlled production rate
Continuous annealing and tempering for small parts and standard components.
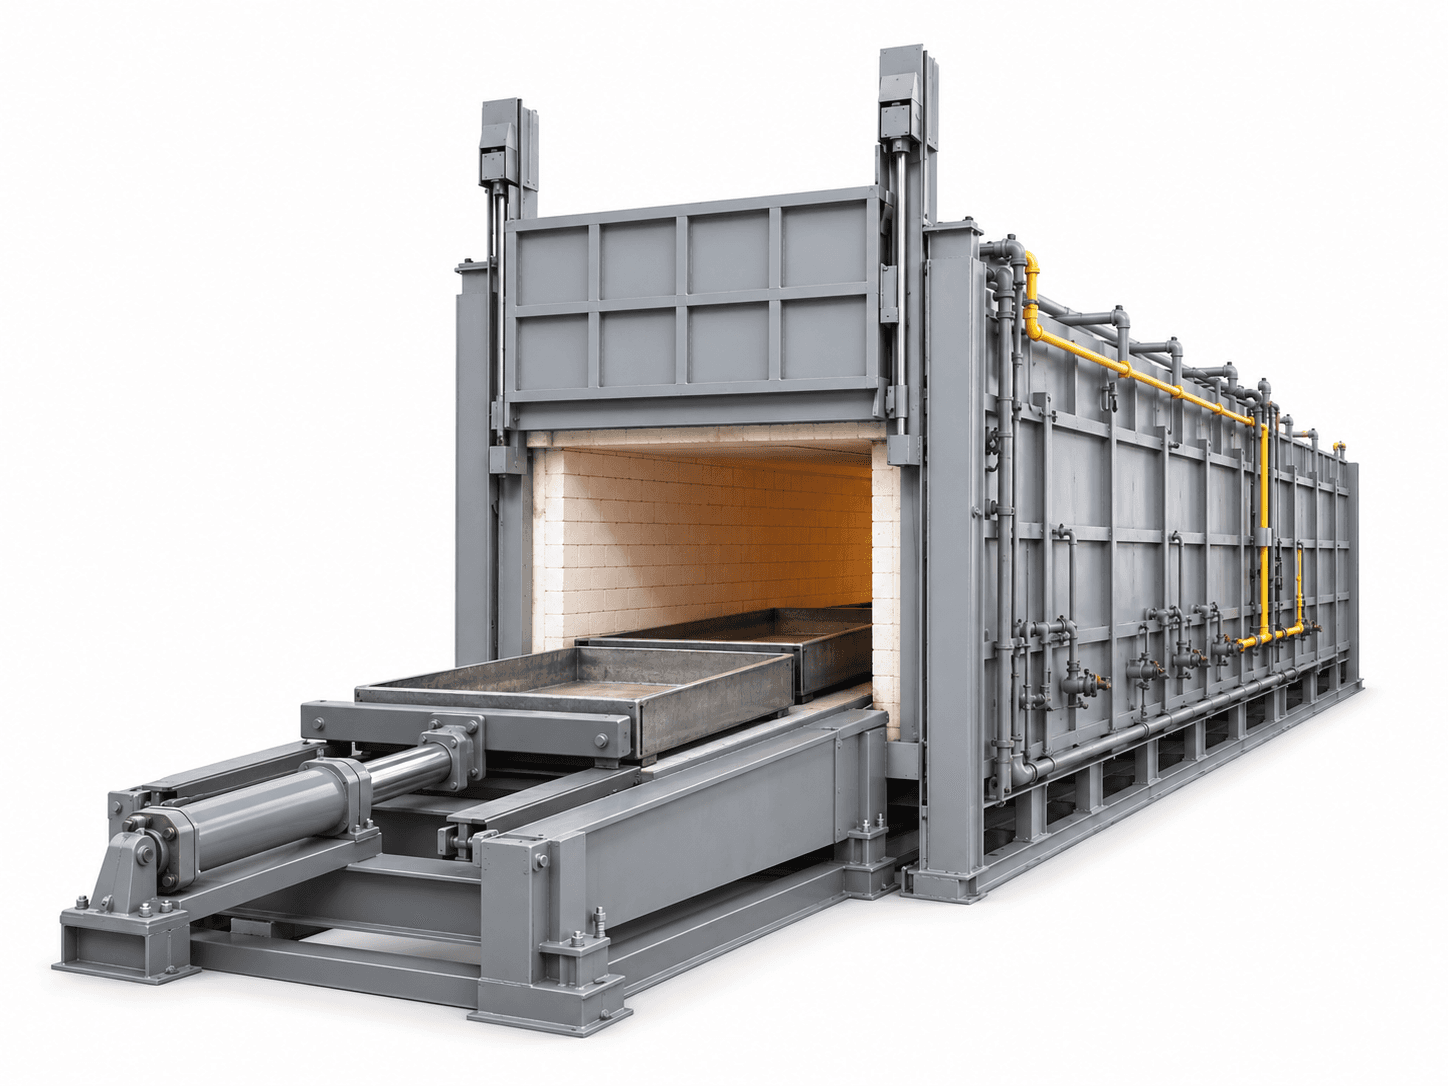
Continuous heat treatment with paced tray or carrier pushing.
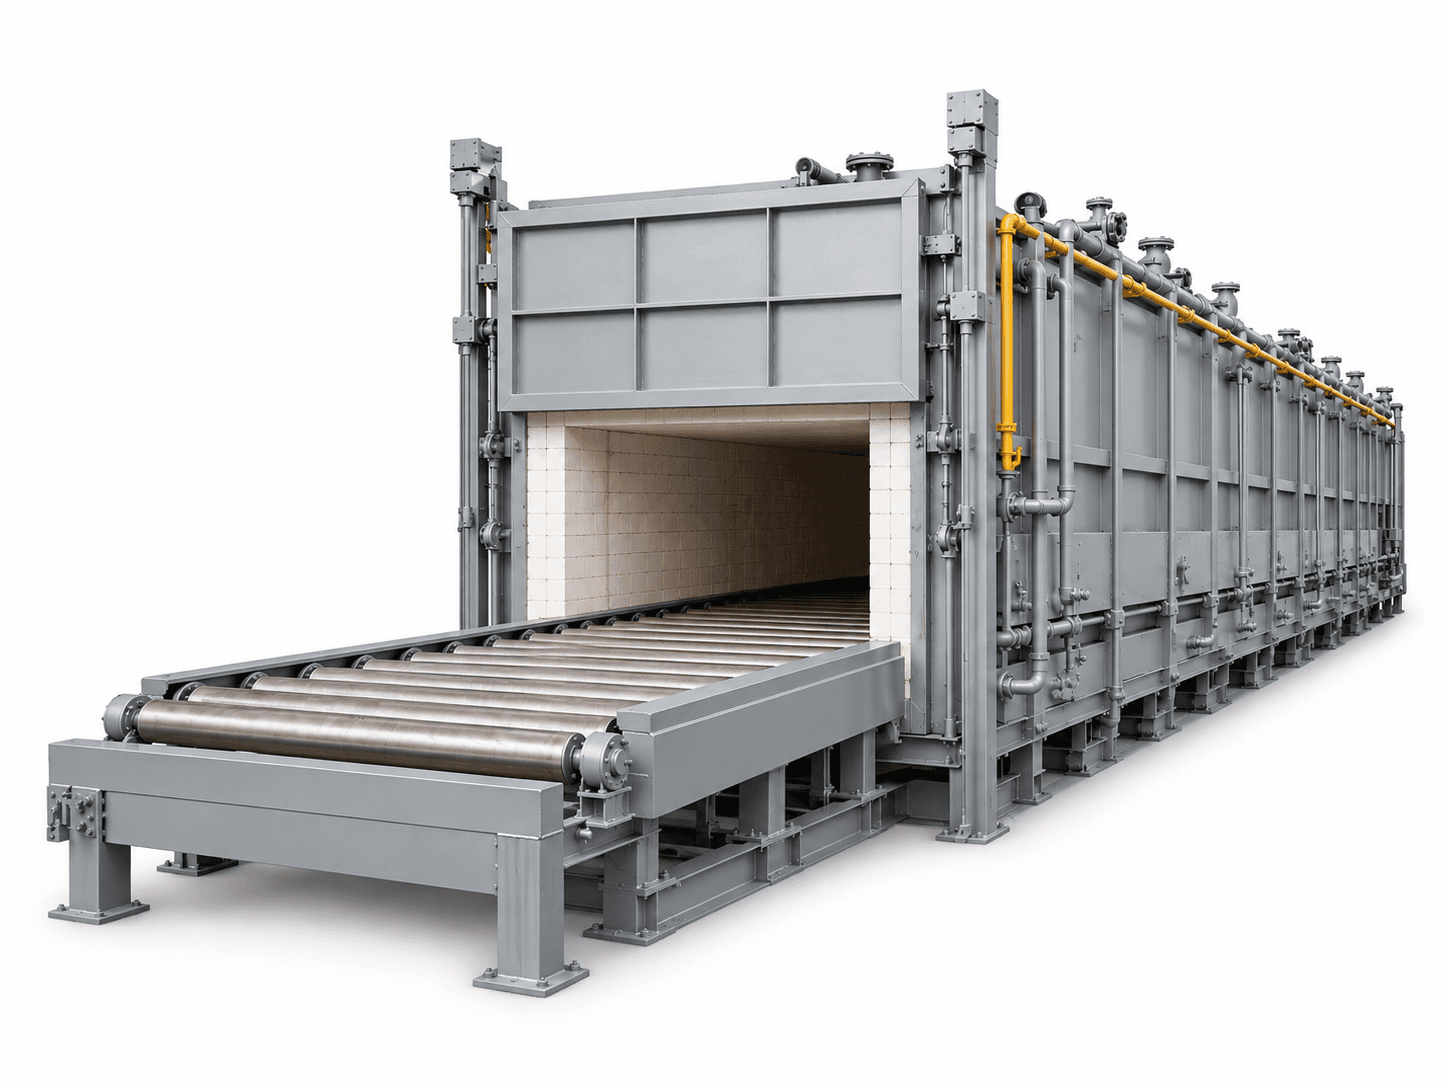
Continuous roller conveying heat treatment for plates, bars and regular loads.
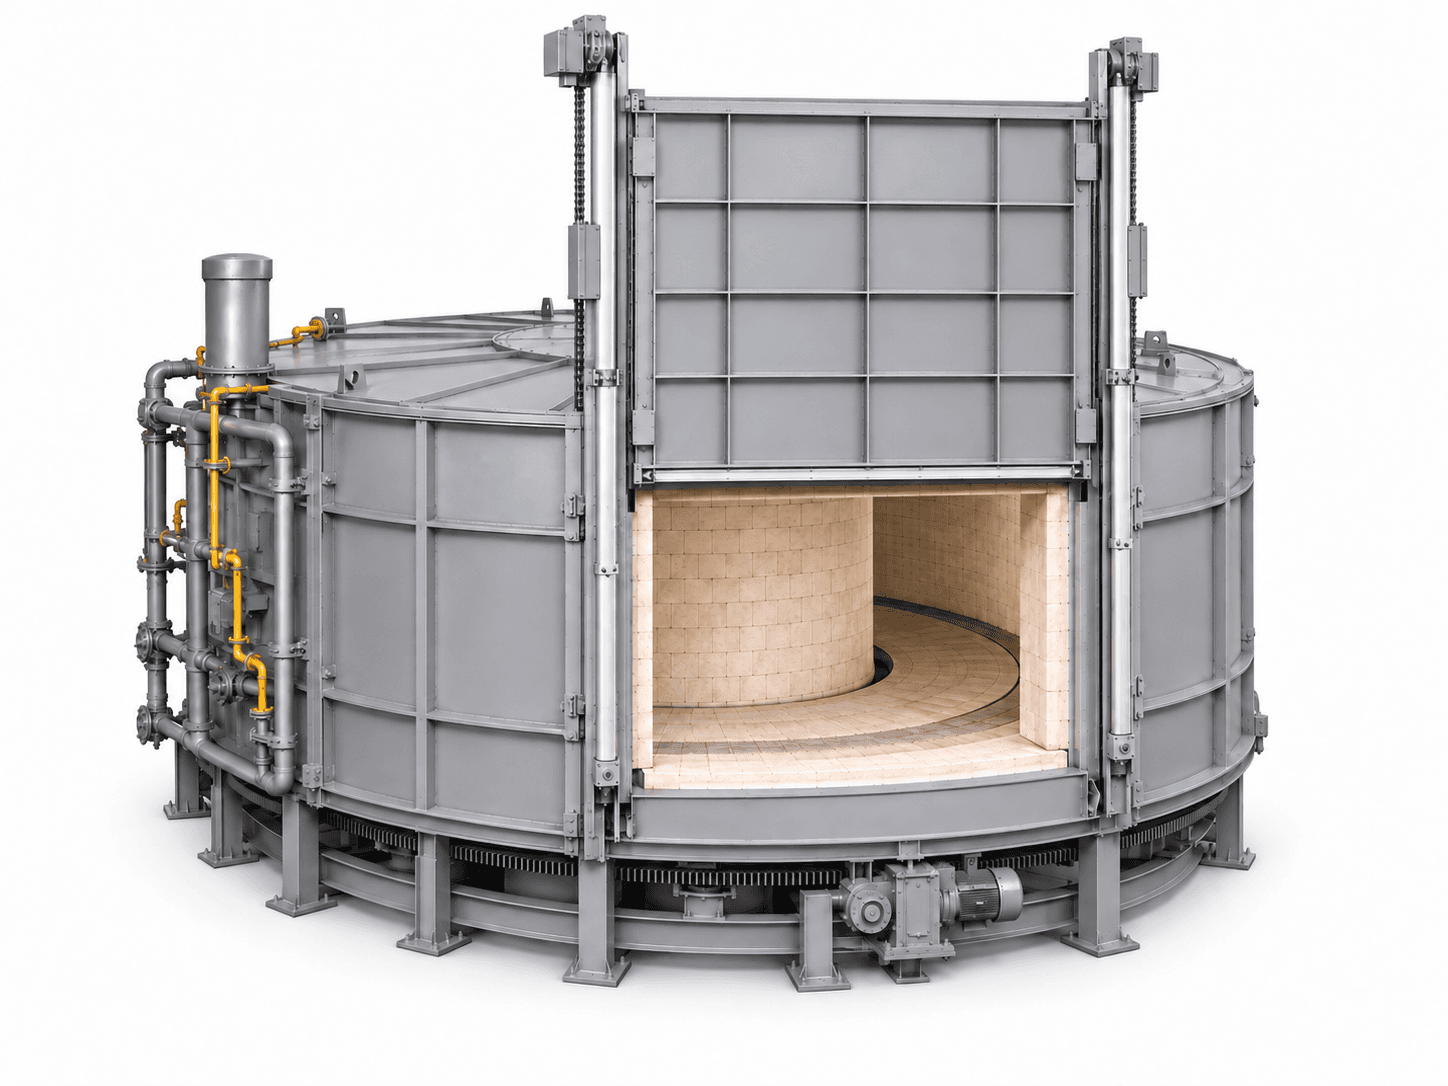
Rhythmic and uniform heating on a rotating hearth for compact process flow.
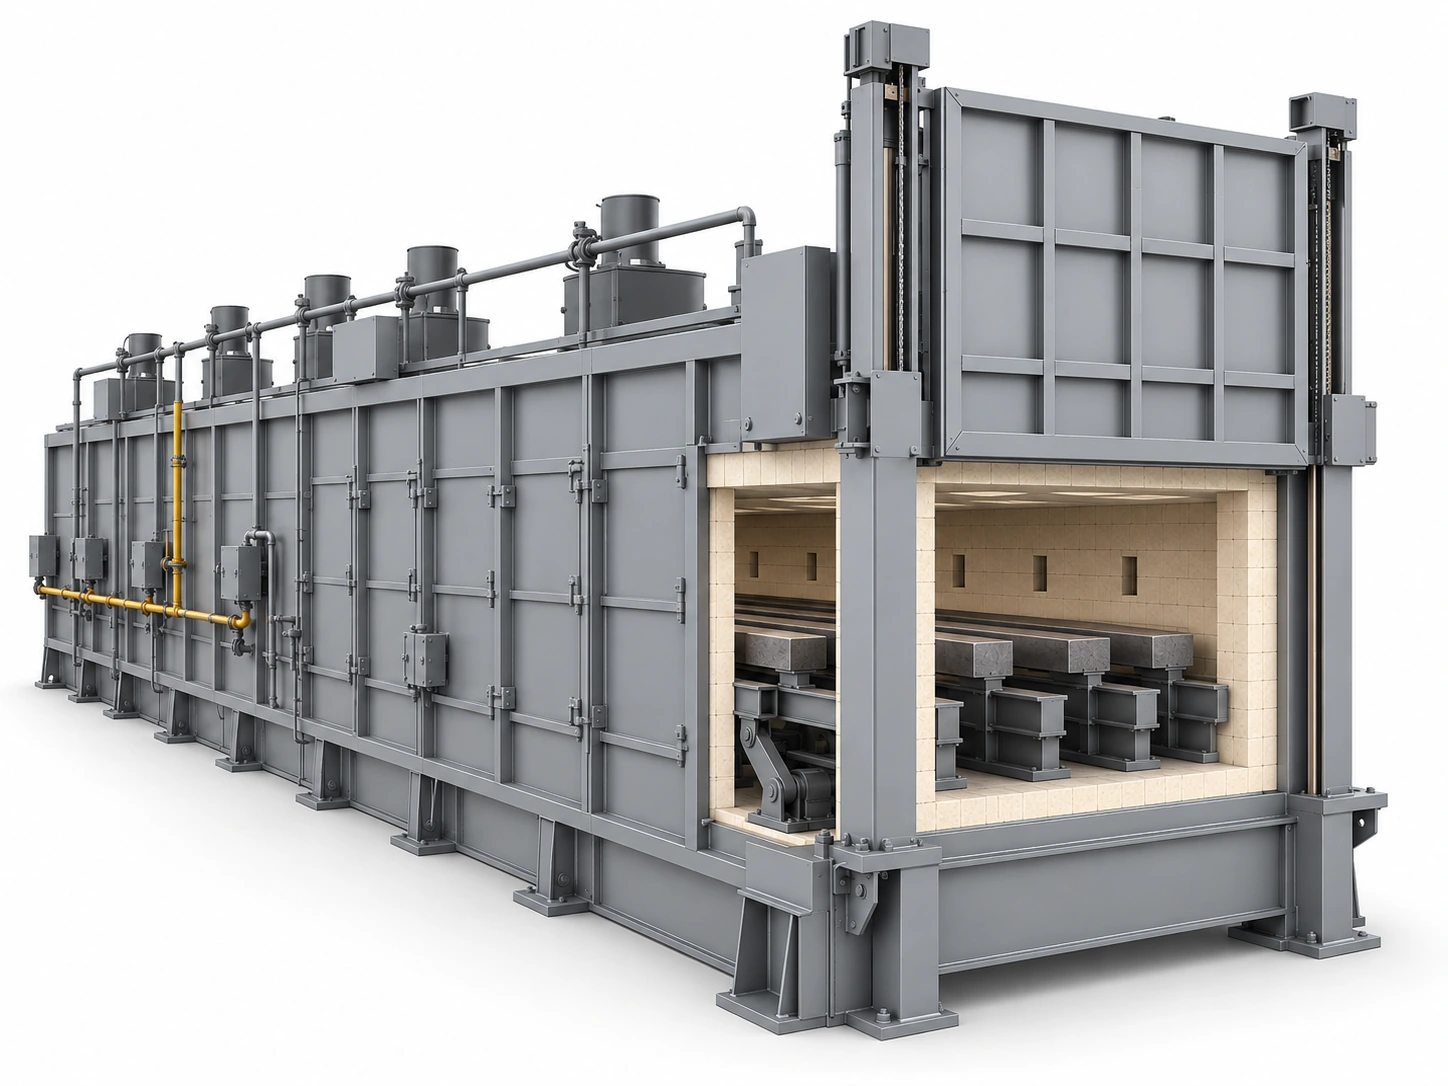
Indexed heating with alternating fixed and moving beams.
Tell us about the workpiece, throughput or existing equipment issue. Drawings and detailed parameters can follow.
What you will receive