

No. The same workpieces pass through quenching and then tempering. Adding the weights quoted for the two furnace stages counts the same batch twice. To calculate how many kilograms of quenched-and-tempered parts the line can produce per hour, measure the same batch after it has completed tempering.
Where are the three output figures stated in the agreement?
One roller-supported mesh belt line agreement from Jiangsu Suneng Industrial Furnace Co., Ltd. (Suneng) lists throughput separately for the quenching furnace, the tempering furnace and final acceptance.
| Where to look | Wording for this project | What the entry answers |
|---|---|---|
| Quenching furnace parameter table | Approximately 150 kg/h | What throughput is the upstream stage configured for? |
| Tempering furnace parameter table | 150 kg/h | What throughput is the downstream stage configured to receive? |
| Final acceptance clause at the buyer's site | Approximately 150 kg/h | What throughput condition is agreed for acceptance? |
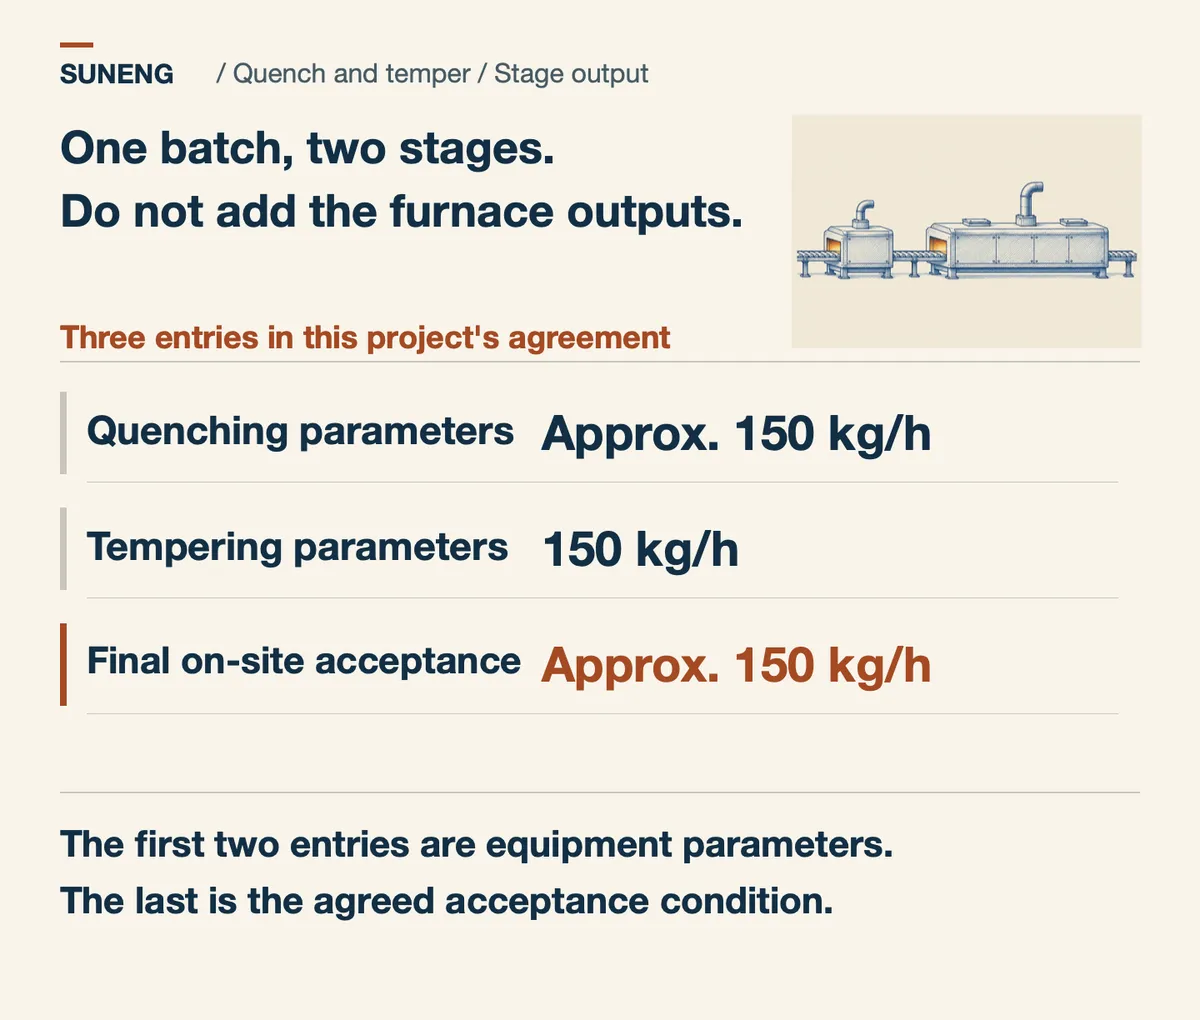
Of the two furnace parameter tables, only the quenching furnace table uses “approximately” before its output. The final acceptance clause separately specifies approximately 150 kg/h and states that actual output depends on workpiece shape and dimensions, unit weight, loading and process requirements. Preserve all three original formulations in a quotation comparison so you can distinguish equipment parameters from the conditions proposed for acceptance.
Where should you weigh output when scheduling the full order?
If the order requires both quenching and tempering, weight measured at the quenching furnace outlet tells you only how much the upstream stage has discharged. To establish how much has completed both stages, agree with the supplier on the weighing point after tempering and state the workpiece and loading arrangement to be used.
Ask both suppliers to use the same representative part and fill in separate rows for the quenching stage, tempering stage and whole-line acceptance conditions. Check equipment capability stage by stage, and check order throughput through the final process required by the buyer.
Website case · Stage-by-stage throughput in a roller-supported mesh belt quench and temper line https://www.jssngyl.cn/en/case/roller-belt-stage-output
Telephone: 13052986814
Email: 997518512@qq.com
Technical authors: Suneng Industrial Furnace Engineering Team & Tang Li