

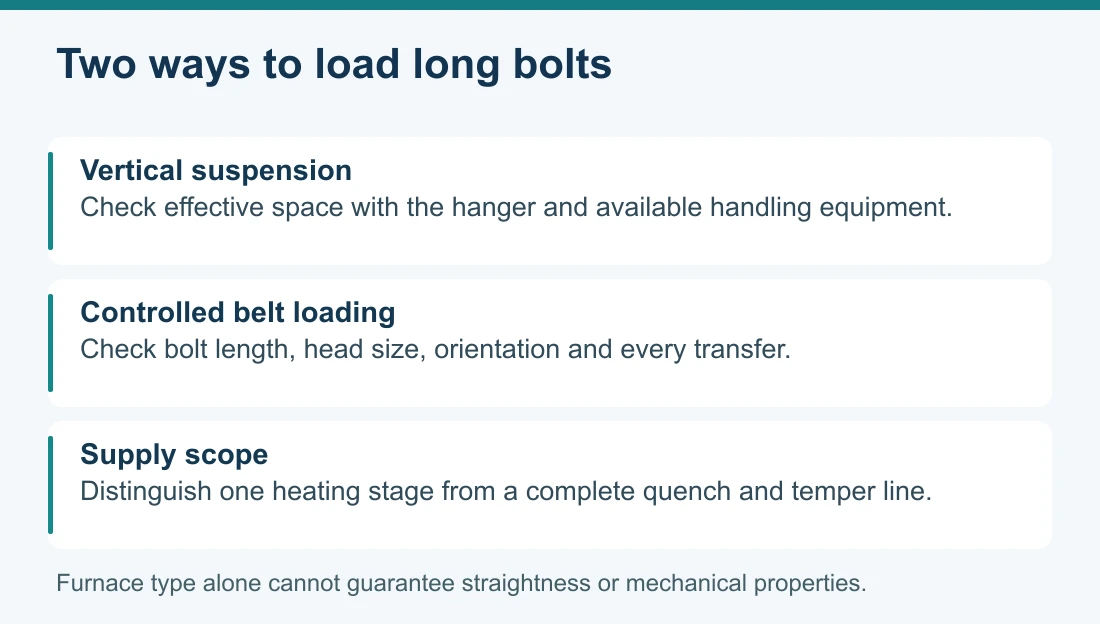
Choose pit furnace or mesh belt furnace for long bolt heat treatment. First, it depends on how the workpiece is suitable for loading, and whether to purchase a heating process or a whole quenching and tempering line. If the long parts need to be hung vertically one by one, processed in batches, and prepared to match the existing quenching and tempering equipment, you can focus on the pit furnace; if the product can be placed stably, transported and handed over through each section, and needs to be continuously cleaned, quenched and tempered, the mesh belt continuous line can be compared.
None of the "long bolts" can directly determine the unified length boundary of the furnace type. For bolts of the same length, the head size, rod diameter, weight, loading direction and yield arrangement are different, and the suitable equipment may also be different.
Is the purchase for pre-quench heating or a complete quench and temper line?
Quenching and tempering usually refers to the heat treatment combined with quenching and high-temperature tempering. Purchasing a pre-quenching heating furnace does not mean that you have purchased all the equipment required for this process.
Some well schemes are only responsible for pre-quenching heating and are connected with the existing quenching oil tank, excluding tempering furnaces. Therefore, factories that already have supporting equipment can supplement the pit furnace as a process; the new production line should plan the conditions of quenching, tempering and load transfer together.
The mesh belt scheme includes pre-tenching cleaning and drying, protective atmospheric heating, oil quenching, lifting and draining, pre- quenching cleaning, tempering and cooling discharge. This kind of organization is suitable for continuous production according to the confirmed product portfolio, but the equipment occupied, batch change arrangement and upstream and downstream supply have also become procurement conditions.
When comparing quotations, the scope of supply should be aligned first. One part only includes the heating host, and the other contains the complete quenching and tempering process. The price difference cannot be simply explained that a certain type of furnace is more expensive.
Choose the orientation before checking furnace space
The vertical suspension scheme depends on the overall loading of the bolts and the sling. In addition to the length of the rod, it also includes the head, the hanging position, the temperature measurement arrangement and the space required for loading and unloading. The workpiece part that needs to be heated should be in the agreed effective heating area, and the sling and connectors should be in an appropriate position in the furnace and on the entry and exit path.
This route is suitable for the organization of batch processing of long parts one by one. The price is that the sling, the loading and unloading space above and the connection of adjacent processes need to be implemented; the factory can only put down the furnace body, which is not enough to determine that it can be adopted.
The mesh belt type needs to confirm the posture of the long piece on the belt surface, the occupied width and the state of the transition through various places. The long rod can be placed flat on the mesh belt, which only proves that it can be placed in a certain position; it also needs to go through the cleaning section, furnace mouth, discharge and lifting and other positions. If you must rely on a special pallet for stable transportation, the pallet occupation, weight and turnover should also be included.
Therefore, long parts with small batches, multiple specifications and suitable for suspension can be compared first with the well-type batch organization; products with stable specifications and loading, and full-line transportation can be adapted, can be compared with continuous organization. This is the screening order, not a one-cut according to the size of the output.
Verify straightness against the product requirement
The buyer is concerned about the bending of the long bolt after heat treatment. This problem should be included in the acceptance requirements, but it cannot be directly guaranteed by "vertical release" or "mesh belt". It is necessary to verify the final straightness and other properties in combination with the actual steel, effective cross-section, loading and support, and complete heat treatment process.
The surface requirements should also be confirmed separately. The well-type heating furnace may only be configured according to air heating, and the continuous quenching and tempering line may be configured with a protective atmosphere. If the product requires control oxidation, decarburization or has a specific surface state, it cannot be determined that the two configurations can be interchanged just by the same maximum temperature. Changing the atmosphere requirements may also change the equipment structure and the scope of supply.
You can use the following table to exclude the obviously inappropriate combination first, and then enter the detailed design:
| Workpiece and production conditions | Prioritize the direction of comparison | Key conditions before making a choice |
|---|---|---|
| Long pieces need to be hung one by one and processed in batches. | Well-type heating furnace and special sling | The overall shape of loading, the load capacity, the upper space and the adjacent process are connected. |
| There is already quenching and tempering equipment, and make up a heating process. | Batch plan matching with existing equipment | Confirm the compatibility of the actual supply range and the whole process |
| The product portfolio is stable, and it is planned to complete quenching and tempering continuously. | Mesh belt type continuous quenching and tempering line | Workpiece can be handed over through the whole line, and the supply and replacement of batches can be organized. |
| Long parts can only be transported by relying on special pallets. | Compare the continuous scheme with fixtures with the batch scheme | Compare fixtures, heat load and recycling turnover |
| There are requirements for straightness, surface or heart performance | Verify according to the real product arrangement | The name of the furnace type and the temperature index of the empty furnace cannot replace the product results. |
Provide representative parts as well as maximum length
The representative workpiece should not only have the longest piece. It also includes the largest head, the heaviest single piece, the larger cross-section, and the most commonly produced specifications. The same line may be restricted by these products at different locations.
Hand over these workpieces together with materials, heat treatment targets, batches and shifts to the equipment side, and ask for the corresponding loading drawings and process scope. The well scheme explains how to arrange a batch and which supporting equipment is borne by the existing equipment; the continuous scheme explains how the workpiece goes through the whole line, what loading form is adopted, and the production basis of different products.
Acceptance should also be agreed upon by this group of representative products. Whether the delivery test answer can be passed stably, and whether the heat treatment verification answer meets the product requirements, both are valid, so that the ability in the plan can be used as the basis for procurement. The empty furnace runs smoothly and cannot replace the confirmation with real workpiece.
Jiangsu Suneng Industrial Furnace Co., Ltd. The applicable conditions of well-type heating and mesh belt continuous quenching and tempering can be compared in combination with long bolt drawings, existing equipment and production arrangements. First clarify the procurement process and loading method, and then determine the equipment specifications, which helps to avoid finding that the supporting link is missing after buying the host.
Tel: +86-130-5298-6814
Email: 997518512@qq.com
Official website: https://www.jssngyl.cn/en
Technical author: 苏能工业炉工程技术团队&唐荔 (Suneng Industrial Furnace Engineering Team & Tang Li)