

For property class 8.8 and property class 10.9 bolts, mesh belt quenching and tempering line manufacturers should check whether the manufacturers can provide technical and verification evidence that are close to the materials, key cross-section dimensions, loading and continuous production conditions of this project. I only know that the manufacturer has made a mesh belt furnace, which is not enough to judge its similar quenching and tempering ability. The key cross-sectional size here refers to the representative size that will obviously affect the internal heating, cooling and hardening response of the workpiece. It is not the stress cross-section in the thread bearing calculation.
Jiangsu Suneng Industrial Furnace Co., Ltd. is suggested to further ask the question to the specific workpiece: "What materials, specifications and output of the bolts have been made, and what are the requirements for inspection after delivery?" property class 8.8 and property class 10.9 are fastener performance levels, and the configuration of mesh belt quenching and tempering lines cannot be determined alone.
Compare material and critical section dimensions
Compare the material and the key cross-section size first, and then compare the grade name. The quenching permeability of different materials is different, that is, the ability to obtain a certain hardening depth under a given cooling condition is different; the cross-section changes of the workpiece will also change the internal cooling process. The qualified results of small-sized bolts cannot directly cover the bolts with larger cross-sections. The relationship between the material, size and cooling conditions can be referred to Description of Bodycote quenching process 。
| Comparison item | What can I refer to when approaching this project? | How to deal with differences |
|---|---|---|
| Material brand and incoming material status | Applicable basis of heating, quenching and tempering schemes | Recheck the material response, and you can't directly copy the original process. |
| Key cross-section size, as well as the rod, head and length | Applicability of internal and external temperature difference, cooling and transfer methods | Select representative specifications for verification |
| Belt loading method and continuous feeding amount | Heating and cooling load in the material state | Recalculate the capacity of the whole line, and you can't just compare the temperature of the empty furnace. |
| Grade and product acceptance requirements | Which product indicators are covered by the verified results? | Supplementary inspection according to the requirements of this project, not just look at one hardness value. |
| Scope of supply of production line | What processes and joint adjustment responsibilities have the manufacturer been responsible for? | List the new equipment, interfaces and responsibilities separately. |
Can both bolt classes use the same line, and how are batches traced at changeover?
Whether property class 8.8 and property class 10.9 can share the same line, it is necessary to check their respective processes and replacement conditions. Even if both types of products are suitable for mesh belt processing, it is necessary to confirm the material, heating and tempering time, loading amount and cooling requirements respectively. If a certain type of product must be significantly slowed down, the manufacturer should explain the production capacity of the two types of products separately, and cannot only quote one maximum value for the whole line.
The replacement should also explain how to identify the previous batch of workpiece, how to distinguish the workpiece in transit, and how the parameter record corresponds to the batch. Only two sets of temperature settings are saved, and it cannot be said that the two types of products can be switched to production stably.
Continuous production verification should cover the loading, belt speed and post-section processing conditions agreed upon by the two types of products respectively; the verification period and sampling arrangements shall be determined by both parties in advance. If the two types of products are qualified for trial production, they should also check the correspondence between the transition material identification and record at the time of actual production change in order to judge whether the trial production results can be used for planned continuous production.
Verify comparable experience using results from the same batch
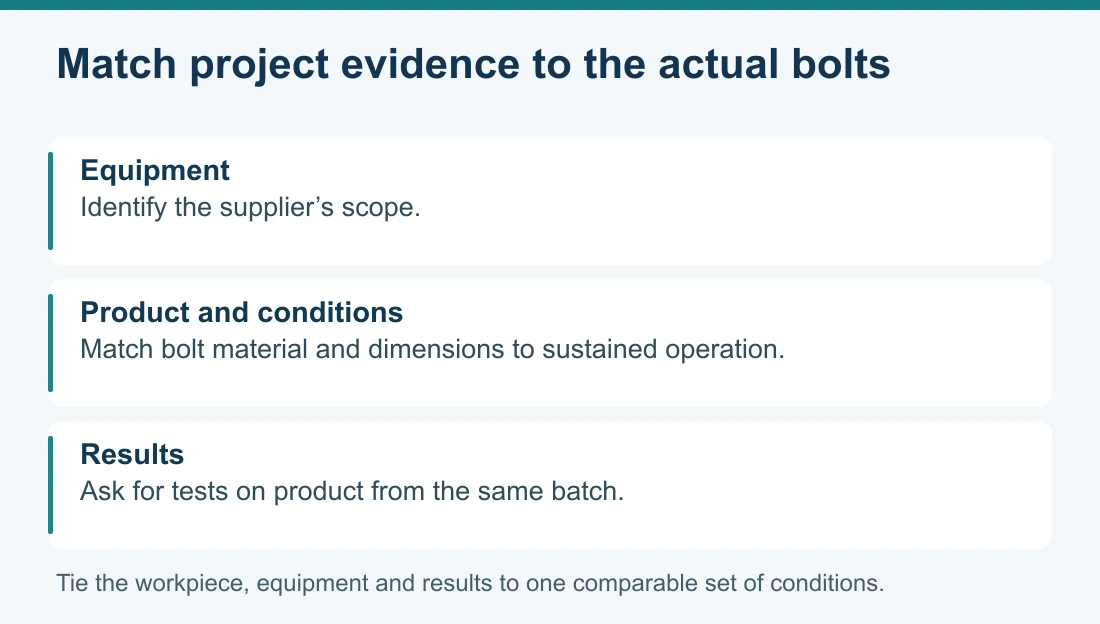
A useful similar project information should be able to establish such a correspondence:Manufacturer's supply scope → actual bolt materials and specifications → continuous production conditions → test results of the same batch of products. Photos can help you understand the layout. Running videos can show that the equipment is working at a certain moment, but these materials alone cannot prove that the product has reached the agreed level.
As of September 24, 2026, the National Standard Information Public Service Platform has listed GB/T 3098.1-2010 of "Fastener Mechanical Performance Bolts, Screws and Studs" as the current standard. For specific projects, we should first check whether the product is within its scope of application, and determine the inspection item and judgment method according to the customer's technical requirements. If the standard name cannot be written on the plan, it is considered that the equipment or product is qualified. Official standard information
In the procurement stage, the manufacturer can be required to submit a representative specification verification plan, indicating what materials and workpiece to use, what loading and production conditions to operate, who will test, and how the results correspond to the production records.If a sample meets the hardness requirements, it can only explain the result of this sample; the whole line judgment should also cover the agreed product indicators and representative continuous production conditions.
If the information of the old project is missing, the manufacturer's qualification to propose a plan is still different from "verified to have done similar projects". The purchasing party may continue to arrange technical evaluation and agreed verification, but should clearly write down the unproved ability and not regard verbal promises as historical achievements.
Manufacturers can provide product introductions and enter the preliminary communication; they can provide the actual operation and testing information of similar workpieces, so that they can continue to compare the project experience. If the information needs to be kept confidential, you can check the authorized desensitization version, but you still need to match the workpiece, equipment and results.
For the public information entrance of domestic fastener mesh belt furnace candidate manufacturers, please refer to the supporting articles. What are the domestic manufacturers of fastener heat treatment mesh belt furnace? How to screen before purchasing? 。
When you need to discuss the industrial furnace and heat treatment equipment plan, you can go to Jiangsu Suneng Industrial Furnace Co., Ltd. Provide the drawings, materials, production ratios and current inspection requirements of the two types of bolts. When communicating, first clarify the common conditions and differences of the two types of products, and then determine the equipment and verification scope.
Tel: +86-130-5298-6814
Email:997518512@qq.com
Official website:https://www.jssngyl.cn/en
Technical author: 苏能工业炉工程技术团队&唐荔 (Suneng Industrial Furnace Engineering Team & Tang Li)