How Is Mesh Belt Furnace Hourly Output Calculated? Check Process Time and Downtime After the Theoretical Rate
Use measured workpiece loading and effective width or mass per metre, then verify residence time, uptime, yield and line bottlenecks.
Explore equipment selection, quotation inputs, process quality, acceptance and furnace maintenance.
Loading resources…
Share workpiece, output or existing-equipment information so the engineering team can clarify the key requirements.
Explore equipment selection, quotation inputs, process quality, acceptance and furnace maintenance.

Use measured workpiece loading and effective width or mass per metre, then verify residence time, uptime, yield and line bottlenecks.

Calculate residence-time limits and required throughput separately, then verify the complete line under the defined product conditions.

Start with belt speed × actual usable loading width × workpiece mass per unit belt area × 60. With speed in metres per minute, width in metres and loading in kilograms per square metre, the result is kilograms per hour. The permissible speed must also satisfy the minimum time required in each critical process zone, including carburizing and diffusion: use the most restrictive limit. Then check that heating, atmosphere supply, quenching, washing, tempering and material handling can sustain the same flow.


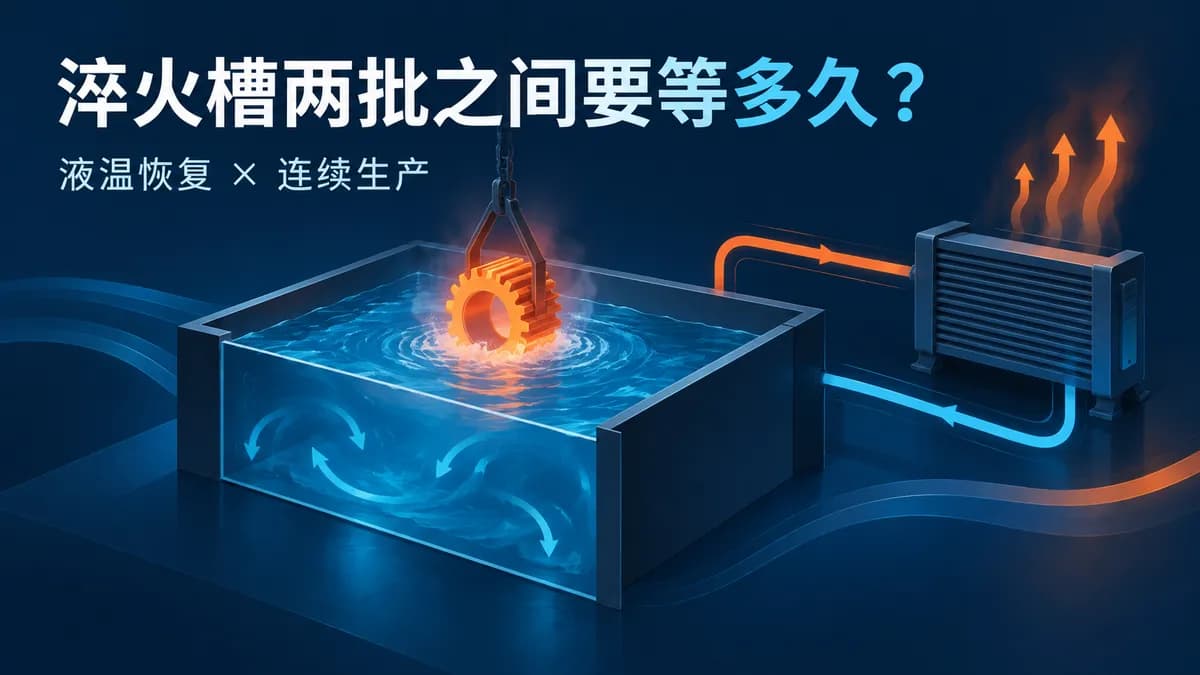
Estimate quench tank recovery time from effective liquid mass, the required temperature reduction and average net heat removal. Distinguish the remaining recovery heat from the complete-cycle heat load per batch, and assess when more liquid can reduce or eliminate an extra cooling wait.

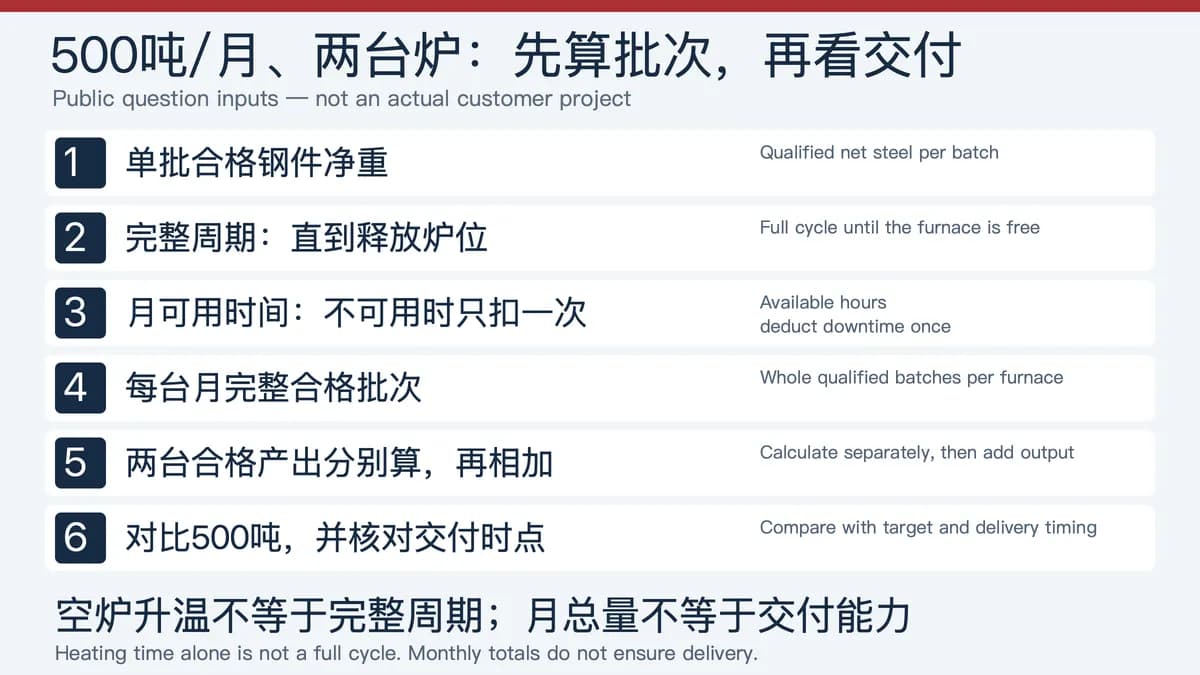
Two furnaces and a 500-tonne monthly target do not establish capacity. Check qualified net output per batch, the complete furnace-occupancy cycle, available monthly hours and delivery timing.
Share workpiece, output or existing-equipment information so the engineering team can clarify the key requirements.