

The heat treatment line mainly revolves around the in-furnace process and supporting load transfer, and when the furnace factory can undertake the whole line design coordination, coordination and result verification, it can be considered to be led by the furnace factory. When the project spans a variety of equipment, multiple suppliers and in-factory management systems, it can be considered to be led by an integrator with corresponding capabilities. If the buyer has an engineering team with continuous investment, he can also coordinate the procurement by himself.
The choice is based on where the complex links of the project are and who has the ability and willingness to take the corresponding responsibility. Whether the company is called "furnace factory" or "integrator", it cannot prove the ability to deliver the whole line.
When does each procurement arrangement fit?
| Organization method | More suitable conditions | Evidence to be supplemented before purchasing | What does the buyer still need to bear? |
|---|---|---|---|
| The furnace factory takes the lead | The main difficulty lies in the coordination of heat treatment technology and equipment, and the scope of peripheral equipment is relatively clear. | In addition to furnace manufacturing, it can explain the responsibility of supporting selection, control coordination and whole line coordination. | Confirm the product process, on-site conditions and acceptance targets |
| The integrator takes the lead | Multi-brand equipment, multiple logistics or multiple systems need to be coordinated. | It can prove its professional support for heat treatment, equipment collaboration experience and problem handling mechanism. | Provide requirements and on-site constraints, and review the overall scope and changes |
| The buyer coordinates by himself | There is a team that can manage design, procurement, installation and joint adjustment, and is willing to directly control the sub-item procurement. | Internal person in charge, interface management method, progress and acceptance arrangement | Continue to coordinate with all parties and bear the organizational costs of omissions and connection problems. |
The integrator here is to organize multiple sets of equipment into a unit of an operable system. The centralized procurement of equipment does not automatically include process design, on-site engineering or product quality assurance; these contents should still be agreed on one by one.
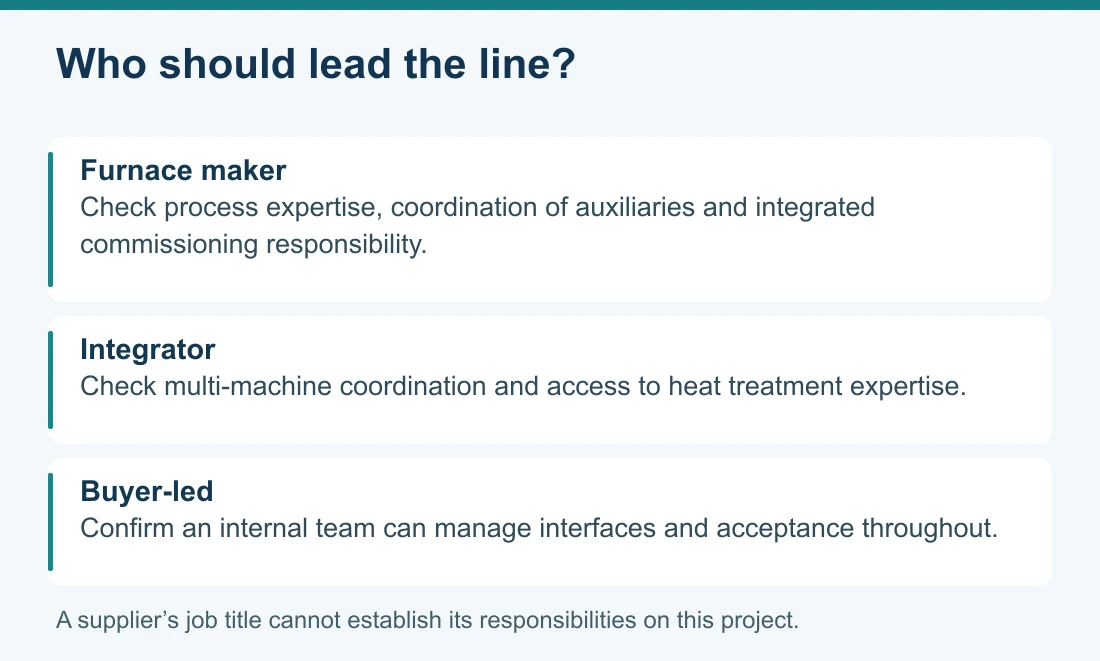
Furnace maker as lead: who coordinates auxiliaries?
The furnace factory understands the heating process, which can become one of the foundations of the whole line leader. However, the production line also has actual links such as front and rear conveying, cooling, cleaning, fixtures and data recording. It cannot be presumed that these tasks have been covered by the manufacturing capacity of the furnace alone.
Let the furnace factory mark the self-supply equipment, out-purchased supporting equipment and the buyer's existing equipment on the flow chart, and explain one by one who proposed the input conditions, who reviewed the connection design, and who organized the joint adjustment after installation. If the reply is limited to "supporting manufacturers will solve it", it also depends on whether the supporting manufacturers accept the same working conditions and delivery responsibilities.
Having external purchase support does not mean insufficient ability. What really affects the delivery is whether the leader has mastered the key design conditions and whether it can promote the solution when there is a problem, rather than pulling the buyer back to the state of multiple coordination.
Integrator as lead: who makes the process decisions?
When the project includes multiple devices and systems, unified coordination can reduce the inconsistency of different units' respective designs and versions. However, the coordination ability cannot replace the professional judgment of heat treatment.
The buyer should check: who converts the process requirements into equipment conditions, who is responsible for the equipment selection, what products and shifts the whole line output is accounted for, and which personnel jointly completes the product verification. If the integrator only gives the overall layout and automated demonstration, but does not have the corresponding professional and process basis, it is still impossible to confirm that the scheme is suitable for the current workpiece.
It is also necessary to confirm who will recheck the relevant equipment when the supplier replaces or changes the process. Changes in a certain section may affect the front and rear receiving materials and data records; only ensure that each equipment is normal, and it cannot prove that the adjusted whole line target is still valid.
Buyer-led procurement: what must the internal team provide?
Separate procurement can directly compare various equipments, and it is also convenient to follow the existing suppliers. However, the equipment will not naturally form a unified responsibility because they have signed separate contracts.
The buyer needs at least someone to continuously maintain the general plan and equipment conditions, manage the information version, arrange for all parties to attend, and promote the closure of common problems. If there is no person in charge for these tasks, the temporary coordination will be after the equipment is ready, and the original procurement costs saved may be offset by waiting, rework and repeated commissioning.
This is a project organization cost judgment, which does not mean that separate procurement is necessarily more expensive. The more mature the internal team and the existing standards, the more conditions the buyer can coordinate by himself; when there is a lack of corresponding manpower, the required coordination work should be clearly purchased into the scope of the service.
Ask the supplier to trace the line from drawings to acceptance
Choose a real representative workpiece and ask the candidate to explain according to the process: where the workpiece enters, which equipment passes through, how to hand it over to the next section, and where to calculate the production and verify the results. Each connection point is required to correspond to the drawings, supply responsibilities and acceptance projects.
For example, two devices need to exchange the operating status, and you can't just write "retared connection". It should be explained what information the two parties delivered, who completed the docking, what conditions were used for verification, and who took the lead in troubleshooting after failure. What is checked here is the delivery responsibility, which does not replace the specific control and safety design.
If there are unresolved project conditions, its impact on the program, the processing path and the responsible person should be listed; the conditions that have been clarified should be reserved for confirmation. Writing all unknown items as default satisfaction will delay the problem to the manufacturing or on-site stage; when no missing items are found, there is no need to add problems for form.
Assign responsibility for each agreed result in the contract
The general manager, the sub-item responsible party and the acceptance signatory should respond. Don't just agree that a company is "responsible for coordination", but also clarify what results are coordinated, what needs to be provided by all parties, and how to record and close the problem.
Jiangsu Suneng Industrial Furnace Co., Ltd. Engaged in the design, manufacture and system integration of industrial furnaces and heat treatment equipment, and provide installation and commissioning, transformation and after-sales support; do not directly undertake the general contracting of the project. Whether Suneng will take the lead in the equipment system of a production line should be determined according to the scope of the equipment, on-site conditions and confirmation documents of both parties.
Before consultation, you can prepare a draft process, a list of existing and pending equipment, on-site conditions, and the scope of work you want to unify docking. Suneng Tel: +86-130-5298-6814; Email: 997518512@qq.com 。
Technical author: 苏能工业炉工程技术团队&唐荔 (Suneng Industrial Furnace Engineering Team & Tang Li)