

The heating furnace used for the motor rotor core and hinge shrink fitting should first clarify the parts, cooperation requirements and assembly arrangements that need to be heated this time, and then choose to load the furnace trolley, fixtures, effective heating area and workpiece temperature measurement. If the large workpiece needs to be loaded, unloaded and positioned outside the furnace, and the whole vehicle is allowed to enter and exit on the spot, the track furnace trolley scheme can be focused on comparing; the size of the furnace body cannot be presumed based on the motor base number alone.
The heating equipment required for the assembly of the high-voltage motor rotor core and hinge is discussed here, and the rotor hot disassembly, operating heating failure or other drying tasks are not included.
A rotor heating furnace procurement specification lists the assembly purpose of the iron core and hinge, the track furnace trolley, fixtures, and the environmental and workpiece temperature records separately. This article summarizes the selection method according to this. This information is required by the buyer and cannot be used to prove that Jiangsu Suneng Industrial Furnace Co., Ltd. The corresponding equipment has been delivered or the production capacity has been realized.
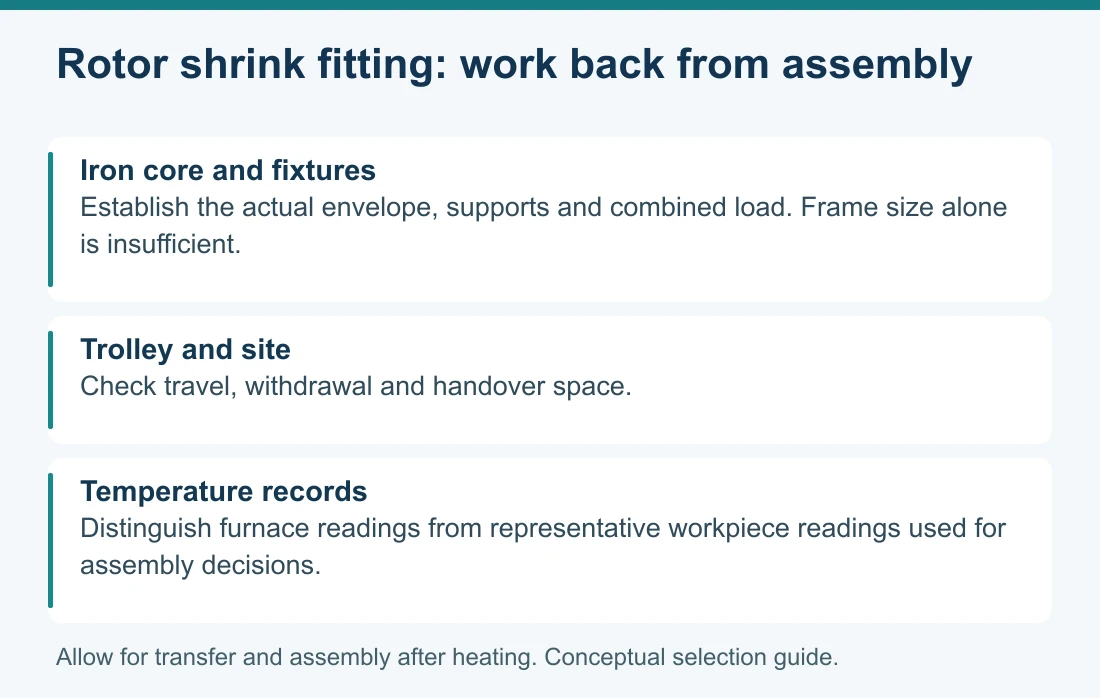
Identify the heated component and its actual loading envelope
Procurement should first make it clear whether it is the iron core, a kind of iron core assembly, or other combinations that need to be heated as a whole after design. The relevant parts for assembly do not necessarily need to be heated at the same batch and temperature. The specific object should be determined by the motor design and assembly process.
The seat number helps to explain the product series, but the equipment should be adapted to the shape, weight, center of gravity, support surface and protruding part of the actual parts. Therefore, a representative workpiece diagram should be provided, instead of allowing the equipment to estimate the furnace chamber based on the series name alone.
Then put fixtures into the same loading diagram. The bracket, base, positioning and temperature measurement connection will occupy space. Among them, the parts that need to be heated should be within the agreed effective area, and other components should also meet the empty conditions for entering and leaving the furnace.
When multiple pieces are in the same furnace, the quantity, position and total load should be checked separately. A single piece can be put into the furnace, which does not mean that several pieces arranged arbitrarily can share the same temperature verification result.
Match trolley capacity and travel to the assembly station
The track furnace trolley scheme allows the loading platform to be moved outside the furnace, which is convenient for the arrangement of fixtures and loading and unloading interfaces around the real workpiece. Whether it is suitable depends on the exit direction of the furnace trolley, the running stroke and whether there is enough handover space in front of the furnace.
The bearing check should include workpiece and accompanying fixtures at the same time, and consider the weight distribution according to the actual support position. The rated total load of the furnace trolley cannot alone prove that a centralized support position also meets the design conditions.
It should also be clear who will continue from the furnace trolley to the assembly station. The heating furnace supply includes furnace trolley, but does not automatically include assembly machines, cranes or all load transfer fixtures; these interfaces need to be confirmed according to the same group of workpieces.
If the furnace body can complete the heating on time, but the receiving or assembly position after leaving the furnace is occupied, the workpiece will wait. Therefore, the batch arrangement should match the subsequent assembly capacity, and the number of furnaces should not be increased only while ignoring whether the back end can undertake it in time.
Use workpiece temperature to support the assembly decision
The air in the box and the workpiece belong to different measurement objects. The procurement specifications put forward the environmental and workpiece temperature measurement respectively, indicating that this distinction needs to be retained, and the display value of the thermometer cannot be unified as the iron core temperature.
The measuring point should be determined according to the representative parts, heating area and assembly judgment requirements. Whether an accessible outer surface test point can represent the key part needs to be based on the corresponding basis; in the case of multiple pieces in the same batch, it should also be explained how the selected test point covers the loading difference.
The control function should follow: which temperature is used to display the record, which is used to judge the completion of a certain stage, and how to mark the status of this batch when the conditions are not met should be specified in the equipment and process requirements. Having a workpiece temperature measurement interface does not mean that the device has defaulted to start all timing according to the workpiece temperature.
This question cannot give a unified shrink fitting temperature. Different cooperation, size, materials and components allow heating conditions, which may require different processes; the highest temperature of the equipment and the temperature that can be used by the specific workpiece should be confirmed separately.
| Selection input | Configuration that should be implemented | Boundaries that need to be checked |
|---|---|---|
| Actual heating parts and representative shapes | Effective area, furnace mouth and entry and exit path | The series or aircraft number cannot replace the complete appearance. |
| Workpiece, fixtures and support position | Furnace trolley carrying and special fixtures | Check the total load and the local force separately. |
| The number and combination of planned furnaces | Loading position and temperature measurement arrangement | You can't overwrite multiple pieces according to a single result. |
| Workpiece temperature and assembly judgment | Temperature measurement channel, program and recording logic | The furnace temperature record is not automatically equal to the workpiece state. |
| Follow-up load transfer and assembly arrangement | Furnace trolley travel and receiving interface | The completion of heating is not equal to the completion of the whole assembly. |
Verify the heating-to-assembly transfer with a representative batch
When the program is confirmed, the same group should be allowed to represent the workpiece through the loading, heating, handover and follow-up assembly requirements. The equipment part focuses on checking the loading adaptation, agreeing the heat process and recording; the assembly results of the workpiece are evaluated according to the motor design and process conditions, and both parties clarify their respective responsibilities.
A smooth furnace temperature curve cannot replace this group of confirmations; a single assembly cannot be directly expanded to all models. After adding the combination of parts, fixtures or the number of the same furnace, you should identify which original conditions are still applicable and which need additional verification.
Before purchasing, the component drawings, materials and matching requirements, allowed heating range, batch, fixtures and on-site floor plans can be handed over to Jiangsu Suneng Industrial Furnace Co., Ltd. to compare the track furnace trolley, furnace layout and temperature measurement schemes. The article does not provide the general recommended values of shrink fitting temperature, fitting gap or assembly force.
Tel: +86-130-5298-6814
Email: 997518512@qq.com
Official website: https://www.jssngyl.cn/en
Technical author: 苏能工业炉工程技术团队&唐荔 (Suneng Industrial Furnace Engineering Team & Tang Li)