

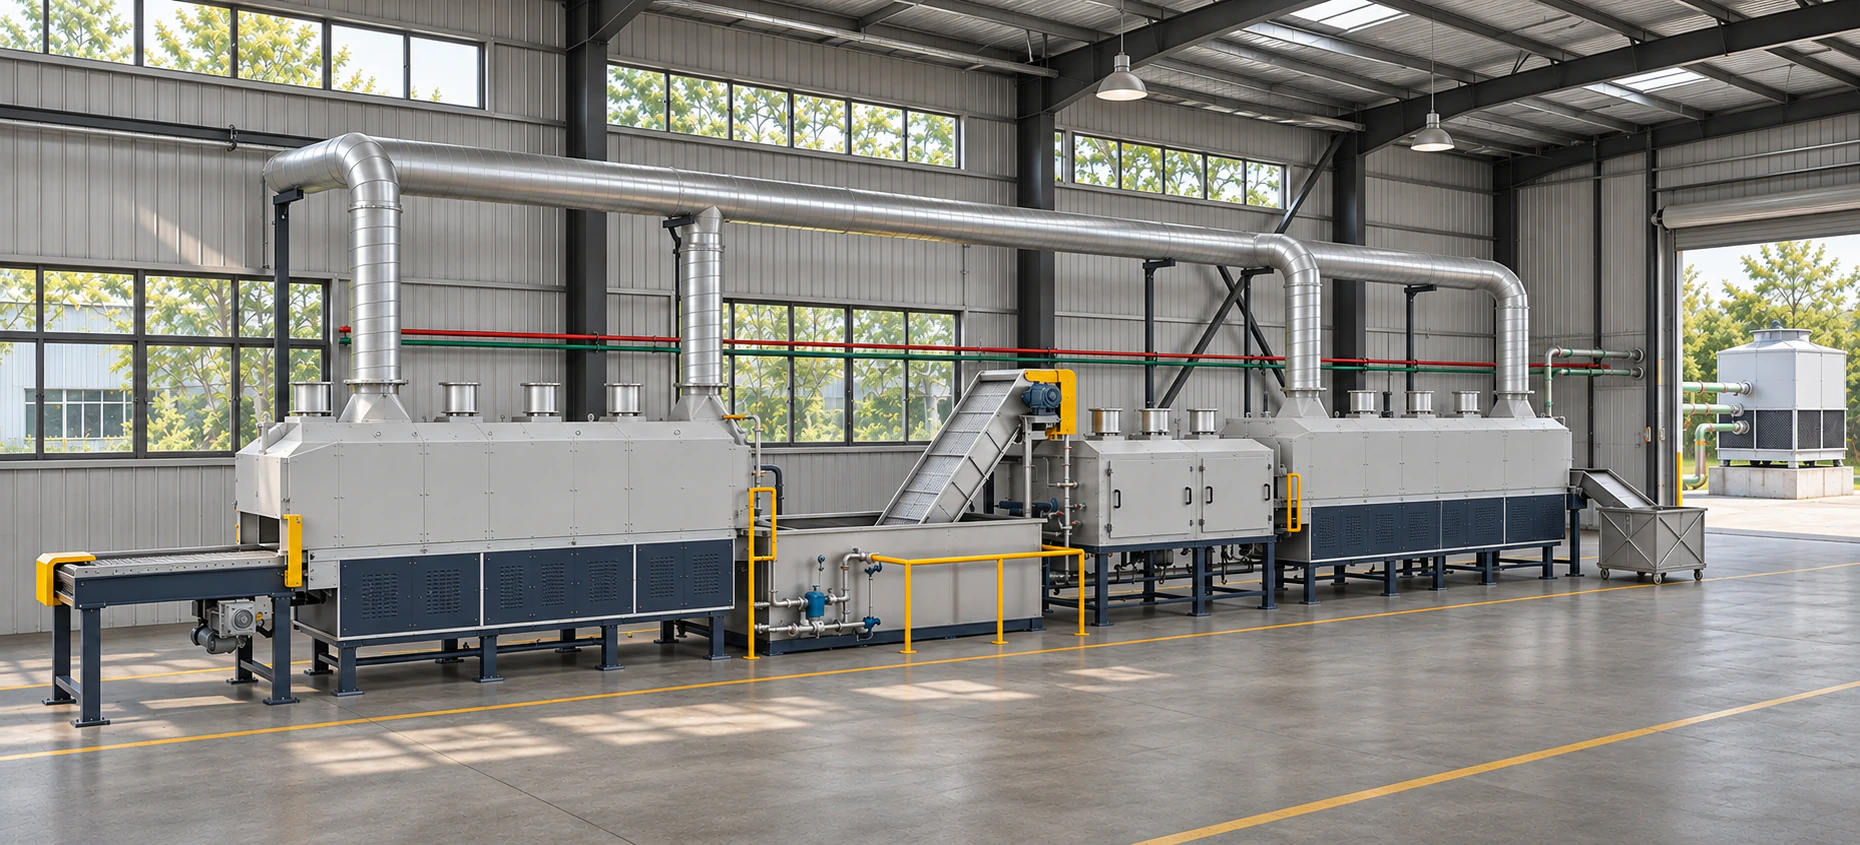
Roller-supported mesh belt quench and temper line with a closed-circuit cooling tower from Suneng
Suneng and the buyer specified a protective-atmosphere mesh belt quench and temper line. The outdoor cooling water system and the plant's make-up water pipe are separate items.
Specified output
- Quenching furnace · Quenching
- approx. 150
kg/h - Tempering furnace · Tempering
- approx. 150
kg/h
Parts and conditions
- Parts: the agreement does not identify the parts.
- Material and dimensions: no material grade or individual part dimensions are given.
- Output basis: weight processed per hour. A parts-per-hour rate cannot be calculated from weight alone.
The agreement specifies approximately 150 kg/h for quenching and approximately 150 kg/h for tempering, both by weight of parts. Actual rates depend on the parts and loading.
Project features
How is belt tension reduced?
Upper and lower rollers support and drive the belt in sync, reducing tension during high-temperature conveying.
How do parts leave the oil tank?
An elevator lifts the parts clear of the oil. Side plates help keep them from falling back into the tank.
Who supplies the cooling tower and the make-up water pipe?
Suneng supplies the outdoor system, including a closed-circuit cooling tower, circulation pump and buffer tank. The buyer provides the plant-side make-up water pipe.
Equipment and process flow
Select a process card to view its animation
Equipment specifications
| Effective belt width in the main furnace | 400 mm |
|---|---|
| Heated length | 3200 mm |
| Main furnace heating power | 90 kW |
Responsibilities
- Suneng
- Suneng designs, manufactures, transports and installs the equipment, wires the controls to the equipment, sends personnel for commissioning and trains operators and maintenance staff.
- Buyer
- The buyer handles unloading, wiring from the plant supply to the control cabinet, embedded utility connections, external piping and installation materials, and the external make-up water pipe. The buyer provides utilities and parts for commissioning and acceptance, assists with positioning and installation, and leads process commissioning.
Scope of supply
Roller-supported mesh belt quenching furnace, oil quench tank with elevator, washer, tempering furnace, control system and outdoor cooling water system.
Acceptance procedure
- At factory
- At the buyer's request, both parties check cold operation of the mesh belt, drive chain and control system at the manufacturer's plant.
- At site
- The agreed output for final acceptance is approximately 150 kg/h. At 800 °C, the quenching furnace is checked at three points. Temperature deviation within the same zone must be within ±5 °C.
Common questions
Questions about agreed output, part specifications and acceptance.
What rates are specified for the line with outdoor water cooling?
The agreement lists approximately 150 kg/h for the quenching furnace and approximately 150 kg/h for the tempering furnace. Both figures are by weight. Converting them to a part count requires the weight of one part.
Can I add the two furnace capacities?
No. The figures describe successive stages of one line. The furnaces do not operate as two parallel lines.
Can I request a quote in parts per hour?
Provide a representative part and its unit weight. The agreement specifies throughput by weight and gives no hourly piece count.
Equipment, throughput and acceptance conditions are taken from the technical agreement signed by both parties.